
Book Appointment Now
Optimizing Cutting Speed and Feed Rate for CNC Efficiency
Cutting speed is how fast the tool's cutting edge moves against the workpiece surface, measured in surface feet or meters per minute. Feed rate is how quickly the tool...
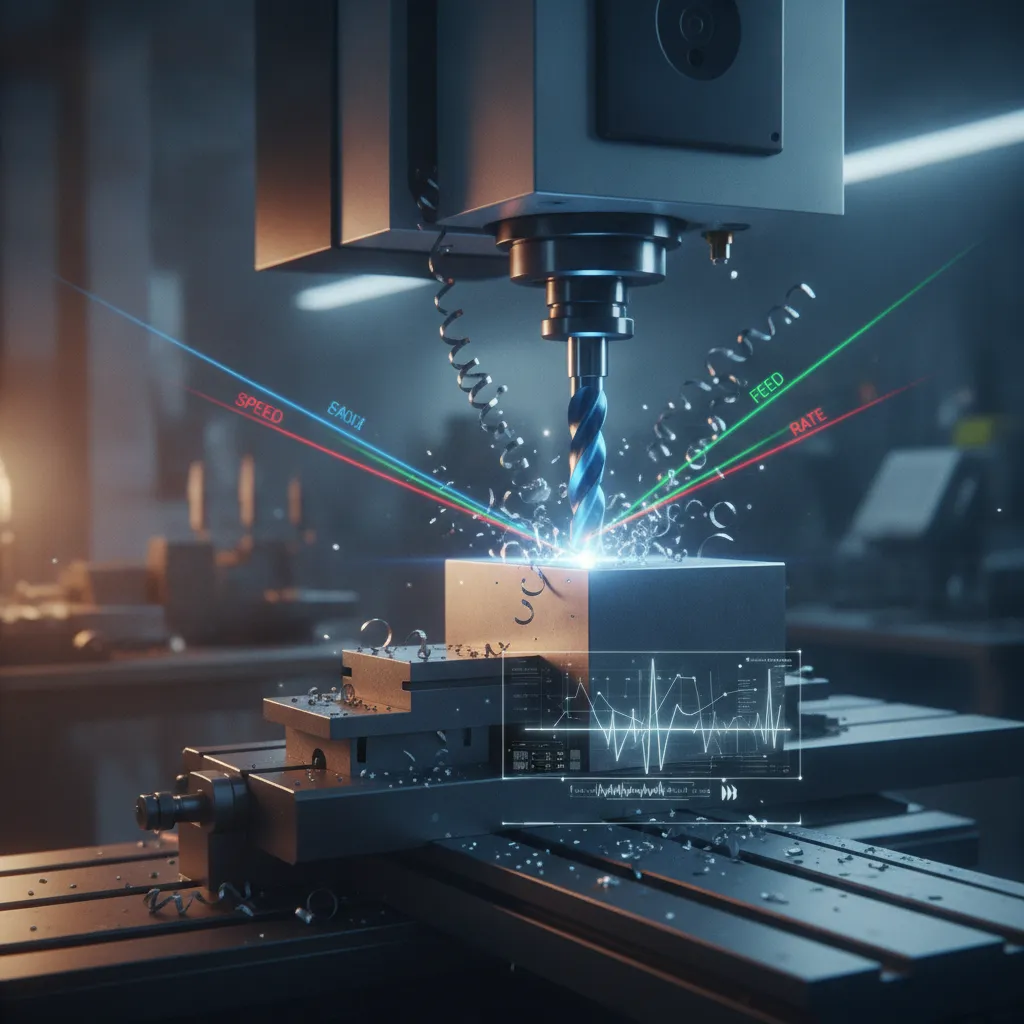
Understanding cutting speed feed rate CNC is essential. Cutting speed is how fast the tool’s cutting edge moves against the workpiece surface, measured in surface feet or meters per minute. Feed rate is how quickly the tool advances through the material, measured in inches or millimeters per revolution or minute. Together, these two parameters control chip formation, heat generation, tool life, and surface finish quality. Getting them right for your specific tool, material, and machine is the single most impactful variable in CNC machining performance.
What Are Cutting Speed and Feed Rate in CNC Machining?: cutting speed feed rate CNC
Cutting speed and feed rate are the two primary motion parameters in CNC machining—cutting speed defines how fast the tool edge contacts the material; feed rate defines how far the tool advances per unit of time or revolution.
What Is the Difference Between Surface Speed and Spindle Speed?
Surface speed (also called cutting speed) measures the velocity of the cutting edge against the workpiece surface, expressed in surface feet per minute (SFM) or meters per minute (m/min). Spindle speed, measured in RPM, is a machine setting—not a direct indicator of how the tool is actually cutting.
The same 3,000 RPM produces a surface speed of roughly 236 SFM on a 0.5-inch diameter end mill but nearly 942 SFM on a 2-inch diameter face mill. Because tool diameter changes the equation, surface speed is the meaningful design target when setting cutting speed feed rate CNC parameters—RPM is derived from it, not the other way around.
Running surface speed too high generates thermal damage at the cutting edge, accelerating tool wear. Running it too low on materials like stainless steel causes work hardening—the material surface becomes harder with each pass, making the next cut progressively more difficult and shortening tool life regardless of other settings.
What Is Chip Load and Why Does It Matter for Feed Rates?
Chip load—also called feed per tooth—is the thickness of material each individual cutting edge removes in a single pass. It connects feed rate directly to tool geometry: a 4-flute end mill at 20 inches per minute carries half the chip load of a 2-flute end mill at the same feed rate.
Feed rate cannot be set independently of cutting speed because chip load determines whether the tool cuts or rubs. An undersized chip load—caused by too slow a feed relative to RPM—means each flute skims the surface rather than shearing a clean chip. That rubbing generates heat without productive material removal, dulling the cutting edge rapidly.
Matching chip load to the tool manufacturer’s recommended range for the material keeps the cut clean, controls heat at the edge, and extends tool life—outcomes that matter whether you are running a prototype or a production batch.
How to Calculate the Right Cutting Speed Feed Rate for Your CNC Project
Two formulas drive every cutting speed feed rate CNC decision: one converts surface speed to RPM, the other derives feed rate from chip load and tool geometry.
Start with spindle speed. The standard RPM formula is:
RPM = (Surface Speed × 3.82) / Tool Diameter
Surface speed comes from your tool manufacturer’s data sheet, it reflects the material pair (tool coating vs. workpiece alloy). The 3.82 constant converts surface feet per minute into a usable RPM figure. Tool diameter is the most sensitive variable: halving the tool diameter doubles the required RPM for the same surface speed, which is why small-diameter end mills spin at 20,000 RPM or more while face mills run at a few hundred.
Feed rate follows directly from RPM:
Feed Rate = RPM × Chip Load × Number of Flutes
Chip load is the thickness of material each cutting edge removes per pass. Flute count amplifies total feed rate, a 4-flute end mill moves the table faster than a 2-flute at identical chip load, but each additional flute also reduces the gullet space available for chip evacuation. In gummy materials like aluminum or copper, fewer flutes often outperform more, because chips clear before they re-cut.
How Do You Find the Sweet Spot for Your Specific Tool and Material?
The sweet spot is the narrow operating band where chip load is high enough to shear material cleanly rather than rub against it, but low enough to avoid deflection or edge breakage. Rubbing below the band work-hardens the surface and accelerates flank wear. Pushing above it overloads the cutting edge, especially when depth of cut is excessive, coolant is absent, or the tool has already lost its edge geometry. For more information, see 5 Essentials For A Killer Retail Marketing Strategy.
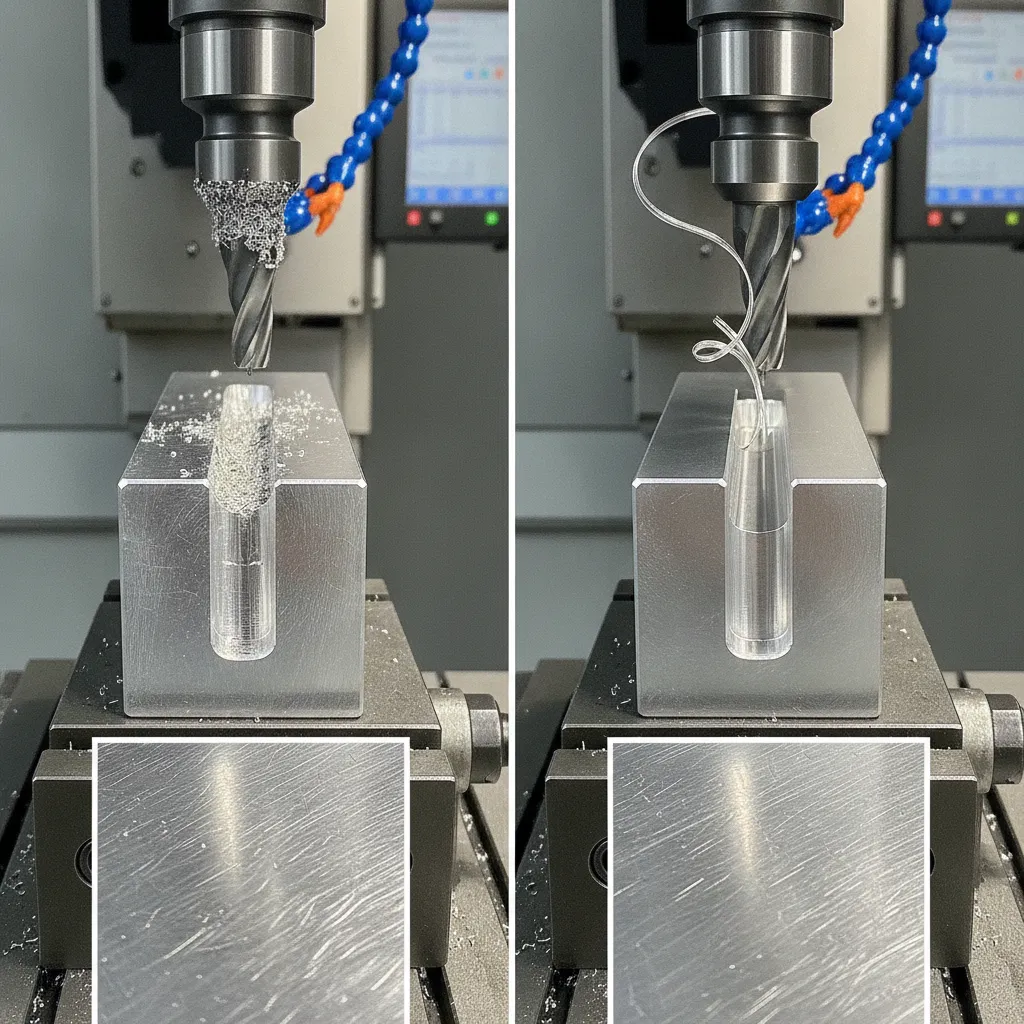
Watch chip color and shape as your primary feedback. Thin, curled, silver chips indicate a healthy cut. Blue or burnt chips signal excessive heat, reduce surface speed first. Powdery chips in metal usually mean the chip load is too low and the tool is rubbing rather than cutting.
What Is the Easiest Way to Use a Feeds and Speeds Calculator?
Treat calculator output as a starting point, not a final answer. Manufacturer data assumes a rigid, well-maintained machine with adequate coolant, conditions that rarely match every shop floor setup exactly. After entering your tool diameter, material, and surface speed, reduce the output by 20–30% if your machine shows any spindle runout, if you’re working with a long tool overhang, or if you’re running dry.
From that conservative baseline, step feed rate up in small increments while monitoring chip formation and spindle load. GC INDUS programmers follow this same iterative approach on 5-axis and Swiss lathe operations, where tool deflection tolerances are tight and a single miscalculated pass can scrap a high-value part.
How Cutting Speed, Feed Rate, and Spindle Speed Work Together in CNC Machines
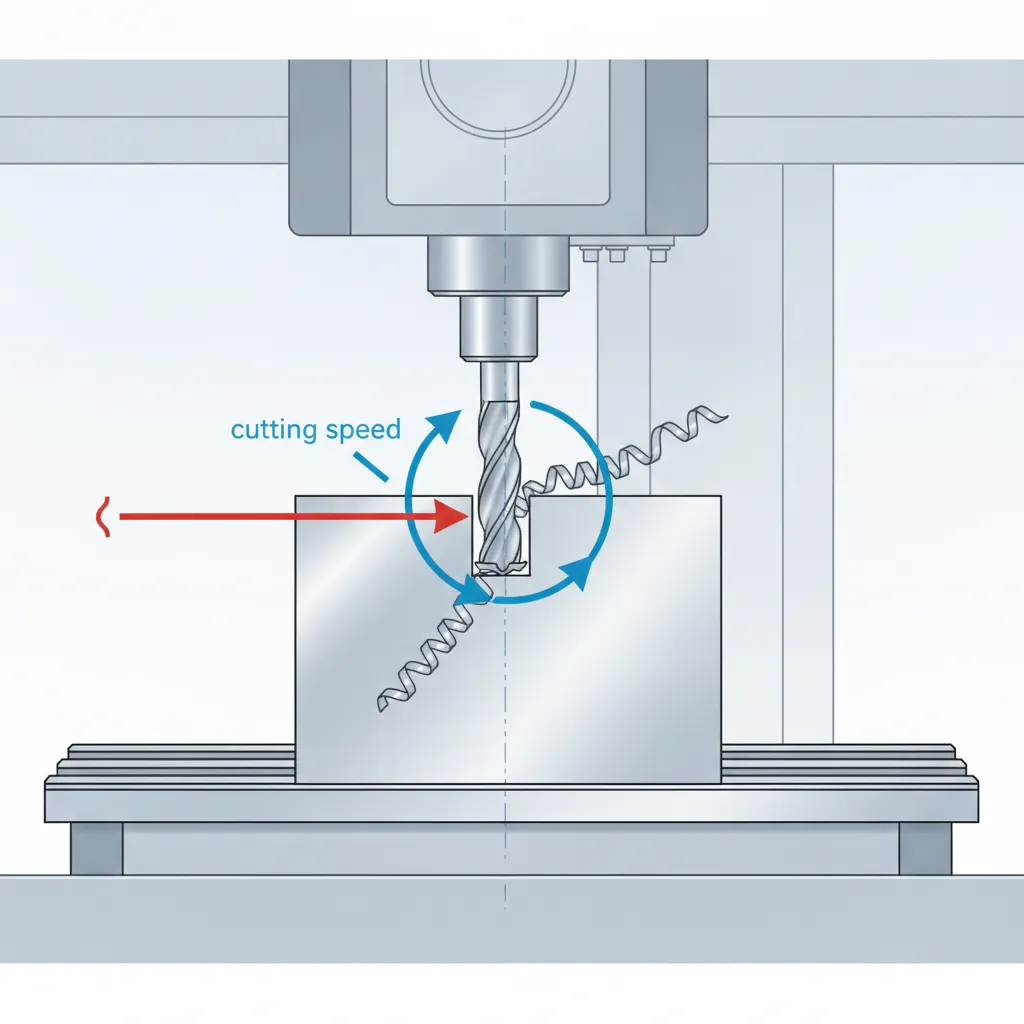
Cutting speed, feed rate, and spindle speed form an interdependent system, changing one without adjusting the others shifts chip load, cutting forces, and surface finish.
Operators who treat these parameters in isolation consistently see shorter tool life and inconsistent part quality. Raise spindle speed without increasing feed rate proportionally, and chip load drops, the tool rubs rather than cuts cleanly, generating excess heat. Raise feed rate without accounting for spindle speed, and chip load spikes, increasing cutting forces until the tool deflects or breaks.
Getting cutting speed feed rate CNC parameters right means treating all three values as a single system, then adjusting for depth of cut and machine type.
How Does Depth of Cut Affect Your Feeds and Speeds Settings?
Both axial depth (how far the tool plunges into the material) and radial depth (how much of the tool’s diameter engages the workpiece) multiply cutting forces directly. A deeper axial cut at the same feed rate increases tool deflection and heat generation, neither of which the original feed rate was calculated to handle.
The compensating adjustment is straightforward: when depth of cut increases, reduce feed rate, cutting speed, or both to keep cutting forces within the tool’s rated limits. Tooling manufacturers publish recommended depth-of-cut ranges alongside their speed and feed tables for exactly this reason.
Why Do Different CNC Machines Need Different Speed Settings?
Machine rigidity sets the ceiling for how aggressively you can run any combination of parameters. A rigid knee mill can sustain higher chip loads than a gantry-style CNC router, where flex in the gantry structure amplifies tool deflection at high cutting forces.
CNC lathes introduce a different dynamic entirely. Single-point turning creates continuous contact between tool and workpiece, generating steady-state heat that behaves differently from the interrupted cuts a rotating multi-flute end mill makes, where each flute briefly contacts the material before exiting and cooling.
CNC routers cutting wood and composites routinely run spindle speeds above 18,000 RPM, far beyond typical metal-cutting mills, because lower material hardness allows higher surface speeds without tool damage. The challenge shifts from heat management to chip evacuation: wood and composite dust must clear the cut zone quickly to prevent recutting and surface burning.
Recommended Feeds and Speeds for Common CNC Materials
Each material’s physical properties, hardness, thermal conductivity, and abrasiveness, set the ceiling and floor for safe, productive CNC cutting speed and feed rate combinations.
Feeds and Speeds for Aluminum, Steel, Wood, and Composites
Aluminum’s low hardness and high thermal conductivity allow surface speeds far above what steel tolerates. The real risk is built-up edge: aluminum welds to the cutting face at improved temperatures, degrading surface finish and breaking tools. Sharp edges, high chip loads, and an aggressive air blast or flood coolant prevent this. Reducing flute count from four to two, or even one, on end mills opens the flute gullet, giving chips a clear exit path before they re-enter the cut and weld.
Steel limits surface speed to protect the tool’s coating from thermal breakdown. Stainless steel adds a second problem: work hardening. When feed rate drops too low, the tool rubs rather than cuts, and that rubbing hardens the material surface ahead of the edge. The hardened layer then accelerates wear on the next pass. Maintaining a feed rate that keeps the tool cutting, not sliding, is the direct counter.
Wood grain direction determines whether fibers cut cleanly or tear. Feeding against the grain produces a cleaner edge; feeding with it on certain species causes fiber pullout. Carbon fiber and fiberglass composites tolerate high surface speeds but generate abrasive particles that destroy uncoated tools within minutes. Climb milling, where the cutter engages the material from the top of the chip, reduces delamination by pulling fibers into the cut rather than lifting them.
How to Adjust Feeds and Speeds When Switching Between Tool Types
Carbide tolerates significantly higher surface speeds than high-speed steel (HSS), so switching from carbide to HSS requires a meaningful RPM reduction, running HSS at carbide speeds overheats and dulls the tool rapidly. Coated tools raise the surface speed ceiling further: TiAlN and AlTiN coatings reflect heat back into the chip rather than absorbing it into the substrate, allowing faster cuts in steel and stainless.
Ball nose end mills require a separate RPM correction at shallow depths. The effective cutting diameter at a given depth of cut is smaller than the tool’s nominal diameter, which means the actual surface speed at the tip is lower than the programmed value. Compensating with higher spindle RPM, calculated from the true engaged diameter, not the shank size, keeps the cutting edge in its productive range. At GC INDUS, tool selection and parameter setting follow this logic across every CNC process, from 5-axis milling to Swiss lathe turning, to hold tolerances to ±0.001mm across production runs.
Troubleshooting CNC Feeds and Speeds: Chatter, Tool Breakage, and Poor Surface Finish
Most CNC feeds and speeds failures trace back to three root causes: chatter, tool breakage, or poor surface finish, each with a distinct mechanism and fix.
How to Fix Chatter, Tool Breakage, and Poor Surface Finish
Chatter is resonant vibration that builds when cutting forces exceed the combined rigidity of the tool, workpiece, and machine structure. The fix is not always to slow down. Reducing radial depth of cut lowers the force that triggers resonance. Increasing feed rate changes the harmonic frequency of the cut. Adjusting spindle speed in small increments, typically 5–10% steps, can shift the system out of the resonant band entirely.
Tool breakage splits into two failure modes that require different responses. Sudden fracture happens when chip load is too high, when the tool enters an interrupted cut without adequate chip thinning compensation, or during a collision. Gradual wear failure happens when cutting speed feed rate CNC parameters push surface speed too high without adequate coolant, accelerating flank wear until the edge collapses. Sudden fracture calls for reducing chip load or feed per tooth; gradual wear calls for reducing surface speed and improving coolant delivery.
Poor surface finish is often a feed rate problem in both directions. Too low a feed rate causes the tool to rub and burnish rather than cut cleanly, generating heat without removing material. Too high a feed rate leaves visible cusps between tool passes. Worn tools produce both problems simultaneously. Chip color and shape are the fastest real-time diagnostic: blue chips in steel signal excessive heat from too-high cutting speed; powdery chips in aluminum indicate rubbing from too-low feed rate.
How Modern CNC Software Adjusts Feeds and Speeds Automatically
Adaptive feed rate control removes the need for an operator to catch these problems manually. Modern CNC controllers monitor spindle current draw as a proxy for cutting force. When the load spikes, typically during roughing passes where stock is uneven, the controller reduces feed rate automatically to keep cutting forces within a safe range. CAM software with adaptive toolpath strategies applies the same logic at the programming stage, varying engagement angle to maintain consistent chip load throughout the cut. The result is fewer tool breaks on variable-stock roughing passes and more consistent part quality without operator intervention.
Frequently Asked Questions
What happens if cutting speed is too high or too low in CNC machining?
Too high a cutting speed accelerates tool wear and can cause thermal damage to both the tool and the workpiece; too low a speed causes rubbing instead of cutting, which also degrades tool life and produces a poor surface finish. The right speed sits in a narrow band determined by the workpiece material, tool geometry, and coating. Running outside that band in either direction raises cost per part—through scrapped tools or scrapped components.
Does coolant affect the feeds and speeds I should use?
Yes—effective coolant delivery allows higher cutting speeds by reducing heat at the tool-workpiece interface. Flood coolant, through-spindle coolant, and minimum quantity lubrication (MQL) each manage heat differently, so the appropriate speed and feed values shift depending on which method you use. Dry machining—common with coated carbide in cast iron—typically requires lower speeds to compensate for the absence of active cooling.
How do I know if my feed rate is correct without measuring equipment?
Chip color and shape are the most immediate indicators: silver or straw-colored chips of consistent thickness suggest a correct feed rate, while blue or burned chips signal excessive heat, and dust-like particles indicate the feed is too low. Sound is also a reliable cue—a steady cutting tone points to stable engagement, whereas chatter or squealing suggests the feed-to-speed ratio needs adjustment. These observations cost nothing and respond in real time.
Can I use the same feeds and speeds for carbide and HSS tools?
No—carbide tools run at significantly higher cutting speeds than high-speed steel (HSS) because carbide retains hardness at improved temperatures that would soften HSS. As a general principle, carbide can operate at cutting speeds roughly three to five times those of HSS in comparable materials, though the exact multiplier depends on grade, coating, and workpiece material. Feed rates may be similar, but speed must be recalculated for each tool type.
Conclusion
Cutting speed and feed rate are not arbitrary starting points—they are calculated decisions that determine tool life, surface finish, and part cost on every CNC cycle. The most actionable takeaways: always derive spindle speed from the manufacturer’s recommended surface speed for your specific material and tool coating, and treat chip formation as live feedback rather than a byproduct to ignore.
For engineers sourcing precision components rather than running machines directly, these parameters matter at the supplier selection stage. A contract manufacturer holding tolerances to ±0.001mm—as GC INDUS does across CNC milling, turning, and 5-axis work—has already optimized feeds and speeds for your material. Request a fast quote and specify your material, tolerance, and finish requirements upfront; that information is what allows a precision shop to return accurate cycle times and pricing from the first conversation.
Recommended Articles
Explore more from our content library:
- <a href="https://gcindus.com/what-is-orthogonal-machining-and-how-it-improves-tool/" title="How Orthogonal Machining Precision Boosts Tool Performance“>How Orthogonal Machining Precision Boosts Tool Performance
- <a href="https://gcindus.com/what-is-tapping-and-threading-in-cnc-machining-and-why/" title="How to Master Tapping and Threading in CNC Precision“>How to Master Tapping and Threading in CNC Precision
- Understanding Batch Production vs. Continuous Manufacturing
- <a href="https://gcindus.com/understanding-burr-removal-in-precision-machining-methods/" title="A Complete Guide to Burr Removal in Precision Machining“>A Complete Guide to Burr Removal in Precision Machining
- What Is DFM (Design for Manufacturability) and Why It


