
Book Appointment Now
Why Additive Manufacturing Precision Engineering Matters
Additive manufacturing precision engineering combines layer-by-layer material deposition with tight dimensional control to produce complex, high-tolerance parts that...
Additive manufacturing precision engineering combines layer-by-layer material deposition with tight dimensional control to produce complex, high-tolerance parts that traditional subtractive methods struggle to match economically. Modern metal additive processes can hold tolerances comparable to many CNC operations, particularly when post-process finishing is integrated. The result is faster iteration, reduced material waste, and the ability to manufacture geometries, internal channels, lattice structures, organic forms, that conventional machining cannot achieve at all.
What Is Additive Manufacturing Precision Engineering and How Does It Differ from Traditional Methods?
Additive manufacturing precision engineering builds parts layer by layer from digital files, enabling complex geometries that subtractive methods cannot produce at comparable cost.
Each layer is fused or sintered onto the previous one, using processes such as selective laser sintering (SLS) or direct metal laser fusion (DMLF), until the part reaches a net-shape or near-net-shape form. This build mechanism fundamentally changes what is manufacturable: internal cooling channels, lattice structures, and organic curves are no longer design constraints but standard outputs.
CNC machining works in the opposite direction. A programmer starts with a solid billet and removes material until the target geometry remains. That approach is highly effective for prismatic parts and tight-tolerance surfaces, but part complexity directly increases machining time, fixturing cost, and scrap rate. With additive processes, a more complex geometry does not automatically mean a more expensive part, the machine deposits only what the design requires.
How Combining Additive and Subtractive Expertise Produces Fully Finished Precision Parts
Additive processes alone rarely deliver the surface finish or dimensional accuracy that critical applications demand. Hybrid manufacturing closes that gap: additive builds the geometry, then CNC finishing, milling, grinding, or turning, brings functional surfaces to specification.
In this workflow, precision engineering means more than a tight tolerance on one feature. It means dimensional consistency across a full production run, verified surface integrity on every mating face, and full material and process traceability, the kind of documentation ISO 13485-certified medical manufacturing requires.
Which Industries Are Being Transformed by Additive Manufacturing Precision Engineering?
Three industries are seeing the clearest impact. Aerospace engineers use additive to consolidate multi-piece structural assemblies into single components, cutting weight without sacrificing strength. Medical device manufacturers print patient-specific implants and surgical instruments in titanium and cobalt-chrome, geometries that casting or machining alone cannot produce. High-performance automotive teams apply the same geometry freedom to optimize cooling passages and reduce component mass in performance-critical parts.
Each of these industries values additive manufacturing precision engineering for the same underlying reason: the ability to manufacture what the design actually requires, rather than what the process will permit.
How Additive Manufacturing Achieves Precision Tolerances and Meets Standards Like ISO 13485 and AS9100
Additive manufacturing reaches tight tolerances through layered process controls and mandatory post-processing, not through the print step alone.
What Tolerance Specifications Can Modern Additive Manufacturing Consistently Deliver?
Four variables govern dimensional accuracy in metal additive manufacturing: laser power, scan strategy, layer thickness, and thermal management. Each one directly affects how much a part shrinks, warps, or deviates from nominal geometry during solidification. Controlling all four within validated parameter sets narrows the tolerance band on non-critical surfaces to roughly ±0.1–0.2 mm for most metal powder bed fusion processes, acceptable for structural geometry but insufficient for mating interfaces or sealing surfaces.
The additive step alone rarely delivers the tightest critical-feature tolerances. Post-process steps close that gap. Stress relief and hot isostatic pressing (HIP) eliminate residual stresses and internal porosity that would otherwise cause dimensional drift. CNC finishing then machines critical bores, threads, and mating faces to tolerances comparable to conventional machining, in some cases as tight as ±0.001 mm, the standard GC INDUS holds across its CNC operations. Surface treatment follows to meet finish requirements the print layer cannot achieve.
Part orientation and support strategy also determine which features hold tightest. Surfaces built parallel to the build plate typically outperform overhanging or unsupported geometry. Designing for additive manufacturing (DfAM) means selecting orientation and support placement to protect the features where tolerance matters most.
How Quality Certifications Enforce Process Discipline in Additive Manufacturing
Additive manufacturing precision engineering only delivers repeatable output when a formal quality framework governs every step. ISO 13485 requires documented process validation and full material traceability for medical device components, meaning each build must reference a validated parameter set, and every powder batch must be traceable to a certificate of conformance. AS9100 adds first-article inspection (FAI), non-conformance control, and supplier qualification requirements that apply equally to additive suppliers in aerospace.
In-process monitoring and end-of-build inspection give buyers the evidence those frameworks demand. Computed tomography (CT) scanning detects internal voids or cracks invisible to surface inspection. Coordinate measuring machine (CMM) verification confirms dimensional conformance against the original CAD model. Material certifications document alloy composition and mechanical properties. Together, these protocols turn a printed part into a documented, auditable deliverable, the standard regulated industries require before a component enters a medical device or aircraft assembly. For more information, see Viticulture De Precision En Medoc Guide Complet.
Cost and Timeline Advantages of Additive Manufacturing Over Subtractive Precision Engineering
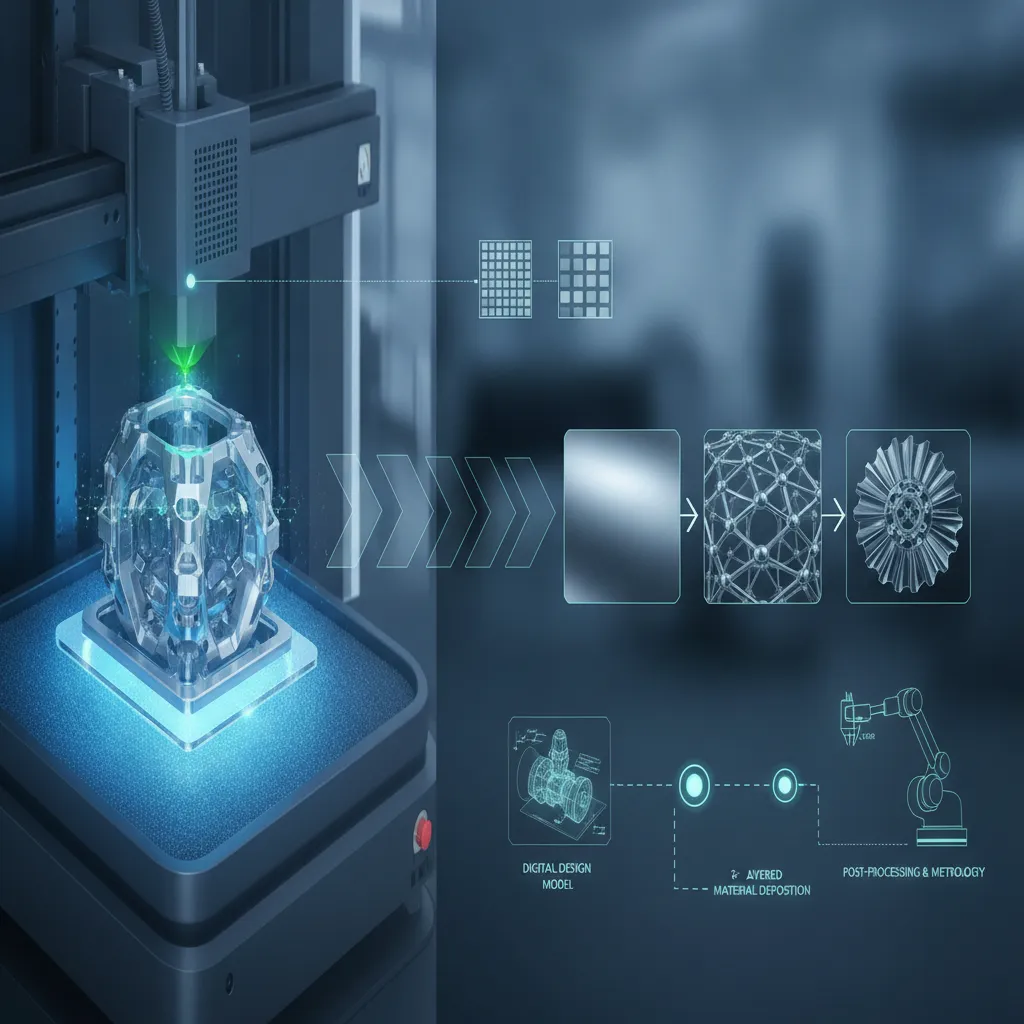
Additive manufacturing cuts upfront cost and lead time by eliminating hard tooling, but subtractive methods still win on high-volume, simple-geometry work.
Subtractive precision engineering typically requires custom fixtures, jigs, and cutting tools for each new part geometry. Designing and fabricating that tooling takes time and budget before a single production part is made. Additive manufacturing eliminates most of that hard tooling, a new geometry means a file update, not a new fixture order.
That mechanism compresses the path from design to first physical part, which matters most during development. When an engineer changes a wall thickness or internal channel, the revision costs a few hours of CAD work rather than days of re-machining a fixture. For low-volume and prototype runs, that speed advantage compounds across every iteration cycle.
When Does Additive Manufacturing Deliver the Fastest Precision Part Turnaround?
Additive manufacturing precision engineering delivers its strongest timeline and cost advantages on complex geometries, low-to-mid volumes, and expensive alloys where billet waste is a significant cost driver.
Titanium is the clearest example. Subtractive machining from billet can waste a large proportion of raw material, additive builds near-net-shape, so far less expensive metal is consumed per finished part. For high-value alloys, that reduction in raw material spend can offset the mid-range to premium per-part machine cost of additive processes.
The comparison is less favorable for high-volume, simple-geometry components. A turned steel shaft produced in thousands of units on a CNC lathe is typically faster and more economical than any additive equivalent. The honest position: additive’s per-part cost often sits at a mid-range to premium tier at low volumes, but total program cost, tooling, material waste, and iteration cycles included, can be budget-friendly compared to a full subtractive setup.
GC INDUS addresses both sides of this equation. For parts where subtractive methods remain the right answer, our CNC milling, turning, and 5-axis machining hold tolerances to ±0.001mm. For programs where additive’s geometry freedom and tooling savings are the priority, understanding which process fits your volume and geometry is the first decision to make correctly.
Which Materials Work Best for Precision Additive Manufacturing Applications?
Titanium alloys, cobalt-chrome, stainless steel, and tool steel are the dominant metals in precision additive manufacturing, each selected for distinct mechanical or regulatory reasons.
How Titanium, Cobalt-Chrome, and Other Alloys Perform in Precision Additive Applications
Titanium alloys (Ti-6Al-4V) are the most widely used metal in additive manufacturing precision engineering for aerospace structural parts and medical implants. The alloy’s high strength-to-weight ratio and proven biocompatibility drive that dominance. Processing demands careful parameter control, however, titanium is highly reactive at improved temperatures, and unmanaged thermal gradients generate residual stress that distorts fine features.
Cobalt-chrome performs where surface integrity under load is non-negotiable. Its wear resistance and corrosion resistance make it the preferred choice for dental prosthetics, surgical instruments, and turbine components. Parts built in cobalt-chrome retain dimensional stability even after repeated mechanical or thermal cycling.
Stainless steel and tool steel grades cover a different set of requirements. Stainless grades handle corrosion resistance in fluid-handling components and medical fixtures. Tool steel grades, chosen for hardness, suit precision tooling inserts and industrial jigs where surface wear would otherwise shorten service life.
Material Efficiency Gains Additive Manufacturing Provides Over Traditional Methods
Near-net-shape additive production significantly reduces the volume of expensive alloy consumed. The buy-to-fly ratio, the mass of raw material purchased versus the mass in the finished part, is a critical cost driver for titanium and cobalt-chrome. Subtractive machining of titanium can produce ratios above 10:1; additive builds bring that figure down substantially by depositing material only where the geometry requires it.
Post-processing requirements vary by alloy and directly affect final mechanical properties. Titanium and cobalt-chrome parts frequently require hot isostatic pressing (HIP) to close internal porosity and achieve consistent density. Specific heat treatment cycles then relieve residual stress and stabilize dimensions, steps that must be factored into tolerance planning from the design stage, not added as an afterthought.
Real-World Results Companies Achieve with Precision Additive Manufacturing Services
Precision additive manufacturing delivers measurable gains in four areas: part consolidation, lead time, component weight, and tooling cost elimination.
Part Consolidation
Additive manufacturing can merge what was previously an assembly of multiple machined components into a single printed part. That elimination removes assembly labour, wipes out tolerance stack-up at mating interfaces, and cuts the number of potential failure points in the finished assembly.
Aerospace and medical device manufacturers pursue this outcome specifically because both sectors carry severe consequences for interface failures. A joint that can crack under vibration or corrode at a brazed seam is a liability; a monolithic printed part removes that risk category entirely.
Lead Time Compression
Moving a design from approval to first inspected part is faster with additive because fixture fabrication and multi-step setup sequences are largely eliminated. A geometry that would require three separate machining fixtures and two setups in a subtractive workflow can go directly from a STEP file to a build platform—shortening the calendar time from days to hours in prototype-to-production transitions.
Weight Reduction in Aerospace and Motorsport
Topology-optimised lattice structures and conformal internal channel geometries are only manufacturable via additive processes. These design approaches remove material from non-load-bearing regions while preserving structural performance along actual stress paths—reducing component mass without compromising stiffness or fatigue life.
What to Look for in a Precision Additive Manufacturing Service Provider
The capability signals that predict consistent results are quality certifications (ISO 13485 for medical, AS9100 for aerospace, ISO 9001 as the baseline), in-house post-processing, full material traceability, and documented inspection infrastructure. A provider without these in place cannot reliably close the gap between a printed geometry and a precision-engineered part.
That gap is closed through a hybrid additive-plus-subtractive workflow—where critical datum surfaces, bore diameters, and mating faces receive CNC finishing after the build. This integration is the deciding factor for regulated-industry applications. GC INDUS applies exactly this model: additive geometry combined with CNC milling, turning, and grinding to ISO 9001 and ISO 13485 standards, with full inspection protocols before any part ships. Additive manufacturing precision engineering delivers on its promise only when the printed form is treated as the starting point, not the finished product.
Frequently Asked Questions
Can additive manufacturing replace CNC machining for precision parts?
Additive manufacturing cannot fully replace CNC machining for the tightest-tolerance precision parts, the two processes work best together. Metal AM builds near-net-shape geometry well, but as-printed surfaces typically require post-process CNC finishing to hit tolerances below ±0.05mm. For parts demanding ±0.001mm accuracy, CNC machining remains the primary process. The strongest production strategies use AM to create complex internal geometry, then apply subtractive finishing to achieve the dimensional control that critical applications require.
What surface finish can you expect from precision additive manufactured parts?
As-printed metal AM parts typically have a rough surface finish, often in the range of Ra 6–25 µm depending on the process and orientation, far coarser than a machined surface. Post-processing steps such as CNC milling, grinding, or electropolishing bring that figure down to Ra 0.8 µm or better. Specifying the required finish before production is essential, because the post-process steps add time and cost that must be planned into the project from the start.
Is additive manufacturing suitable for low-volume precision production runs?
Yes, low-volume production is one of the strongest applications for additive manufacturing in precision engineering. AM eliminates tooling costs that make small CNC or casting runs expensive, so producing 1 to 50 complex parts can be economically viable. The trade-off is per-part cycle time, which is slower than high-volume subtractive methods. For prototype-to-pilot-run quantities with complex geometry, AM often delivers faster results and lower total cost than traditional tooled processes.
How does part orientation during additive manufacturing affect dimensional accuracy?
Build orientation directly controls where support structures are needed, how staircase stepping appears on curved surfaces, and how residual stress distributes through the part, all of which affect final dimensions. A feature printed vertically may hold tighter tolerances than the same feature printed at a shallow angle, where layer steps create measurable deviation. Engineers experienced in Design for Additive Manufacturing (DfAM) evaluate orientation early in the design phase, because a poor choice can require extensive post-machining to recover accuracy.
Conclusion
Additive manufacturing earns its place in precision engineering when it is matched to the right geometry, material, and tolerance requirement, not applied as a default replacement for proven subtractive processes. The clearest takeaway: use AM to build complexity that CNC cannot reach, then finish with machining to hit the dimensional tolerances your application demands. Second, specify post-processing requirements before the first layer prints, because surface finish and accuracy targets shape the entire production plan.
If you are evaluating whether a specific part design is a candidate for AM, hybrid production, or conventional CNC machining, submit your CAD file to GC INDUS for a fast quote, the review will identify which process combination holds your required tolerances at the lowest total cost.
Recommended Articles
Explore more from our content library:


