
Book Appointment Now
Electropolishing Precision Parts for Better Surface Quality
Electropolishing is an electrochemical finishing process that removes a thin, uniform layer of metal from precision parts, leaving a microscopically smooth...
Understanding electropolishing precision parts is essential. Electropolishing is an electrochemical finishing process that removes a thin, uniform layer of metal from precision parts, leaving a microscopically smooth, corrosion-resistant surface. Unlike mechanical polishing, it works from the inside out, dissolving microscopic peaks and burrs at the surface level without introducing stress or directional scratches. For precision components in medical, aerospace, and industrial applications, it delivers cleaner geometry, improved corrosion resistance, and tighter functional performance than most mechanical alternatives.
What Is Electropolishing and How Does It Work on Precision Parts?
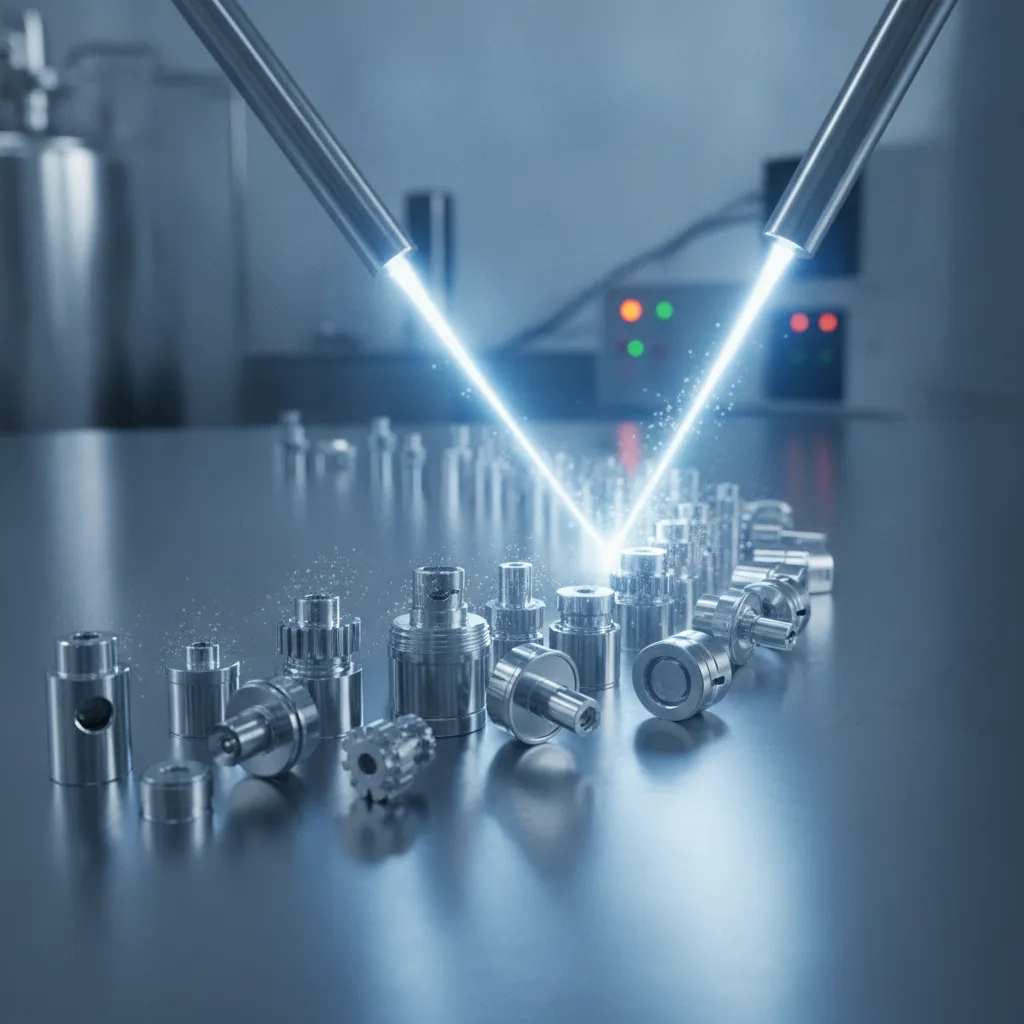
Electropolishing uses direct electrical current to dissolve a controlled layer of metal from a part’s surface, leaving it smooth, bright, and corrosion-resistant.
The part is submerged in an electrolyte bath, typically a blend of phosphoric and sulfuric acids, and connected as the anode in an electrolytic cell. A cathode, usually stainless steel or copper, completes the circuit. When current flows, metal ions dissolve from the part’s surface. The critical detail is that current density is highest at surface peaks, called asperities, because they protrude closest to the cathode. Those peaks dissolve faster than the recessed valleys, which gradually levels the surface and produces the characteristic bright finish associated with electropolishing precision parts.
Process engineers control four primary variables: current density (typically measured in amps per square foot), bath temperature, electrolyte concentration, and immersion time. Adjusting any one of these shifts the rate and uniformity of material removal, which is why process qualification matters before running production quantities.
How Does Electropolishing Improve Surface Finish on Machined Parts?
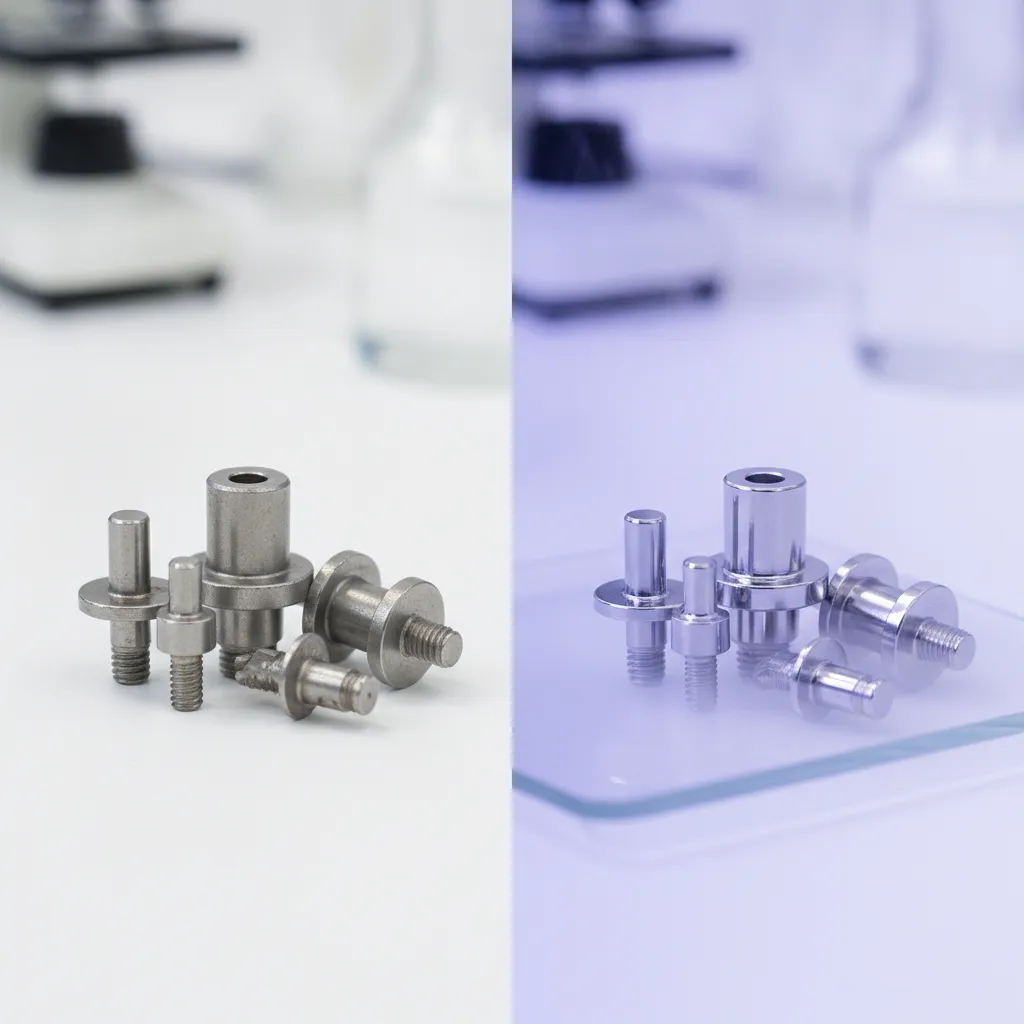
Removing asperities directly reduces Ra, the average surface roughness value measured in microinches or micrometers. A lower Ra means fewer micro-peaks where corrosion initiates, bacteria accumulate, or friction concentrates. For parts with tight dimensional tolerances, this matters because the improvement comes from material removal, not from smearing or compressing the surface as mechanical abrasives do. The process is non-contact, so it introduces no mechanical stress, no directional scratch pattern, and no risk of smeared metal closing off internal pores or cross-holes.
That non-abrasive character is what separates electropolishing from grinding or lapping. Mechanical methods can alter surface microstructure and leave residual stress. Electropolishing dissolves material at the atomic level, preserving the underlying grain structure.
What Are the Disadvantages of Electropolishing Manufacturers Should Know?
Electropolishing removes material uniformly across the part, typically between 0.0002 and 0.001 inches per cycle, depending on process settings. That means the machined part must be dimensioned with this stock removal factored into the final specification before finishing begins. Applying electropolishing to an already out-of-tolerance part will not correct the deviation; it will move the dimension further from nominal.
This is why electropolishing belongs in the process plan from the design stage, not added as an afterthought. At GC INDUS, finishing steps including surface treatment are integrated into the manufacturing sequence, so final dimensions account for any material removed during post-machining operations.
Which Metals and Chemicals Are Compatible with Electropolishing Precision Parts?
Stainless steel, titanium, aluminum, copper, and brass are the metals most compatible with electropolishing; the electrolyte chemistry must match the specific alloy.
The electrolyte solution is the foundation of the process. For austenitic stainless steels—grades 304 and 316L being the most common—phosphoric-sulfuric acid blends are the standard formulation. Aluminum, copper, and titanium each require different electrolyte chemistries tailored to how their surface oxides dissolve under anodic current. Specifying the wrong chemistry for the alloy produces uneven material removal or surface damage rather than a polished finish.
Austenitic stainless steels respond well because their chromium and nickel content supports a stable, uniform dissolution front. Titanium and its alloys are well-suited where biocompatibility and corrosion resistance are priorities—a common requirement when electropolishing precision parts for medical or aerospace applications. Aluminum alloys, copper, and brass also respond predictably, provided the electrolyte is correctly formulated for each.
Which Metals and Alloys Are Not Suitable for Electropolishing?
Cast iron, carbon steel, hardened tool steels, and assemblies with dissimilar-metal welds are poor candidates for electropolishing.
Cast iron and carbon steel are prone to pitting because their microstructure—graphite inclusions in cast iron, carbide phases in carbon steel—dissolves at a different rate than the surrounding matrix, leaving a rough, cratered surface. Hardened tool steels present a similar problem: the high carbide content disrupts the uniform dissolution the process depends on. Parts with welds joining dissimilar metals create localized galvanic differences that cause preferential attack at the weld interface rather than controlled polishing.
Do You Need to Passivate After Electropolishing?
Electropolishing stainless steel typically produces a chromium-rich passive oxide layer as a direct result of the process, which often eliminates the need for a separate passivation step.
The anodic dissolution preferentially removes iron from the surface, leaving a chromium-enriched layer that is more corrosion-resistant than the base alloy. For most stainless steel applications, this built-in passivation is sufficient. A separate post-process passivation—typically a nitric or citric acid treatment per ASTM A967—may still be specified when a customer’s quality standard explicitly requires documented passivation as a discrete step, or when the part will be used in a highly aggressive chemical environment where the additional oxide thickness provides a measurable margin. For more information, see Viticulture De Precision En Medoc Guide Complet.
Electropolishing vs. Passivation, Mechanical Polishing, and Other Finishing Methods
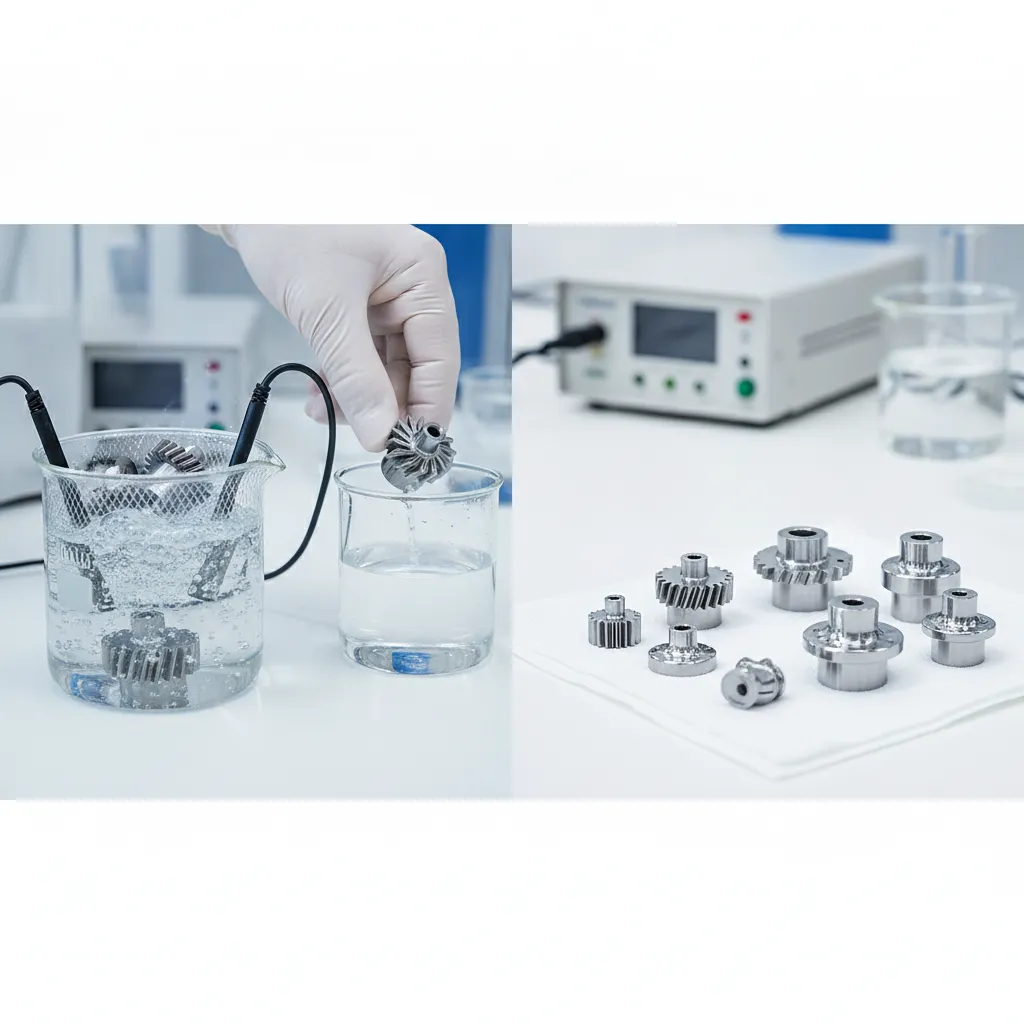
Electropolishing outperforms most alternative finishing methods on surface cleanliness, corrosion resistance, and geometric reach—but each method has conditions where it is the right choice.
Passivation and Mechanical Polishing Compared Directly
Passivation uses nitric or citric acid to dissolve free iron and form a chromium oxide layer on stainless steel. It improves corrosion resistance without touching surface topography. Electropolishing does both simultaneously—it removes surface metal anodically while producing the same passive oxide layer, leaving a smoother, cleaner profile.
Choose passivation alone when a part has an acceptable surface finish and only needs its oxide layer restored after machining or welding. Choose electropolishing when the part also carries burrs, micro-peaks, or contamination that passivation cannot address.
Mechanical methods—grinding, buffing, and lapping—remove material directionally. That direction creates a surface “lay,” smears inclusions into the substrate, and introduces residual stress. Electropolishing removes material isotropically, dissolving peaks uniformly across the entire surface, including internal channels and recessed features that a buffing wheel or lap plate cannot physically reach.
Pros and Cons of Electropolishing vs. Vibratory Finishing and Chemical Polishing
Vibratory finishing excels at deburring and edge-breaking on high-volume, simple-geometry parts. It is cost-effective and fast. On complex geometries, however, media cannot reach internal passages, and the process cannot match the corrosion resistance or cleanliness that electropolishing precision parts demands in medical or aerospace applications.
Chemical polishing uses acid immersion to smooth surfaces without electrical current. It is simpler to set up but offers less process control, produces less consistent Ra improvement, and does not provide the same level of ionic surface cleanliness.
When Should You Choose Electropolishing Over Alternative Finishing Methods?
Electropolishing is the right choice when parts have complex internal geometries, require medical-grade cleanliness, operate in corrosion-critical environments, or cannot tolerate the mechanical contact that grinding or buffing would impose on thin-walled or close-tolerance features.
Avoid electropolishing when parts have deep blind recesses that trap electrolyte—rinsing becomes unreliable and residual acid risks damage. Dissimilar metal assemblies are also problematic, since different alloys polish at different rates in the same bath. Finally, if the controlled material removal conflicts with final dimensional requirements on a tight-tolerance feature, the finishing sequence must be planned before electropolishing is specified—not after.
What Affects the Cost of Electropolishing and How Is It Priced?
Electropolishing cost is driven by part geometry, alloy type, batch size, required finish specification, and turnaround time—not a single flat rate.
Part geometry is the most immediate variable. Simple flat or cylindrical parts process predictably; components with internal channels, blind holes, or complex contours require longer immersion cycles and more precise electrolyte control, which increases labor and process time. Part size matters too—larger surface areas consume more electrolyte and tank capacity per piece.
Alloy selection also shapes cost. Standard 300-series stainless steel processes in widely available electrolyte formulations. Titanium, Nitinol, and specialty nickel alloys require tailored chemistries and tighter process controls, which adds to the per-part cost. The tighter the surface finish specification—measured in Ra values—the longer and more controlled the cycle must be.
Pre-process requirements add to the total. Parts must arrive dimensionally correct and clean. Any pre-cleaning, masking, or custom fixturing the finisher performs is billed as additional work. For electropolishing precision parts with tight dimensional tolerances, arriving in spec is non-negotiable—the process removes material, and an out-of-tolerance blank will only move further out of spec.
Turnaround Times and Batch Processing Capabilities for Electropolishing
Standard batch scheduling is the most cost-efficient route for non-urgent production runs. Expedited processing—where your parts jump the queue or run as a dedicated batch—typically carries a premium. If your program allows lead time flexibility, building electropolishing into the standard production schedule avoids that surcharge entirely.
How Batch Size and Volume Affect Electropolishing Cost
Electropolishing is a batch process. Setup time, electrolyte preparation, and handling are largely fixed costs per run. Spreading those fixed costs across a larger quantity of parts lowers the per-unit price at volume. Small prototype or sample runs carry a higher per-unit cost because the same setup overhead applies to far fewer pieces.
Positioned against basic mechanical finishing, electropolishing sits at a mid-range to premium tier. That cost difference, though, often offsets downstream expenses—reduced rejection rates, elimination of a separate passivation step, and extended service life in corrosive or high-purity environments. For medical device and aerospace components, the total cost of ownership calculation frequently favors electropolishing over cheaper alternatives that require additional finishing steps.
Which Industries Use Electropolishing and What Are the Real-World Applications?
Medical devices, aerospace, semiconductor equipment, and food processing are the four sectors that specify electropolishing precision parts most consistently—each for distinct functional reasons.
Medical Devices
Surgical instruments, implants, and fluid-handling components are routinely electropolished because the process addresses three simultaneous requirements: surface cleanliness, corrosion resistance in body-fluid environments, and reduced bacterial adhesion. Fewer surface asperities mean biofilm has fewer anchor points—a direct structural argument for specifying the process on any implant or instrument that contacts tissue or blood.
Aerospace and Defense
Fatigue life is the governing concern on high-cycle components such as fasteners, hydraulic fittings, and structural brackets. Electropolishing removes surface stress risers and micro-cracks that would otherwise serve as initiation sites for fatigue fracture under cyclic loading. Eliminating those initiation sites extends service intervals and reduces the probability of in-service failure on safety-critical hardware.
Semiconductor and Cleanroom Equipment
Electropolished stainless steel surfaces outgas less and clean more completely than mechanically finished alternatives—both critical requirements in wafer fabrication and pharmaceutical manufacturing where particle counts and trace contamination directly affect yield and product sterility.
Food, Beverage, and Pharmaceutical Processing
FDA and EHEDG cleanliness standards drive electropolishing adoption on product-contact surfaces. Smooth, burr-free surfaces resist product buildup and are easier to validate for clean-in-place (CIP) protocols, reducing the risk of contamination between production runs.
How Electropolishing Improves the Fit, Function, and Reliability of Critical Metal Parts
Removing burrs and micro-peaks changes the contact geometry of mating surfaces. In moving assemblies, this reduces friction and wear at the interface. In precision fits, eliminating those peaks tightens the effective functional clearance—the part performs closer to its designed tolerance than a mechanically finished equivalent would, even when both measure within the same nominal specification.
Frequently Asked Questions
Can electropolishing be used on parts with complex internal geometries or blind holes?
Electropolishing works on internal geometries, but electrolyte flow and current distribution are the limiting factors. Channels, bores, and through-holes that allow adequate fluid circulation can be polished effectively. Blind holes and deep recesses present a real challenge—electrolyte stagnates, current density drops, and the finish becomes uneven. Specialized fixturing, auxiliary electrodes, or flow-through tooling can address some of these cases, but each geometry needs individual assessment before committing to the process.
How much material does electropolishing typically remove from a precision part?
Electropolishing removes between 0.0002 in and 0.001 in (roughly 5–25 µm) of material per surface in a standard cycle. The exact amount depends on current density, bath temperature, and dwell time. Because removal is uniform and predictable, engineers account for it in the pre-polish tolerance. Parts destined for electropolishing are typically machined slightly oversized to preserve final dimensional compliance.
Is electropolishing a replacement for passivation on stainless steel parts?
Electropolishing is not a direct replacement for passivation, but it produces a superior chromium-oxide-rich surface layer that meets or exceeds the corrosion resistance passivation achieves. ASTM B912 and ASTM A967 both recognize electropolishing as an acceptable passivation method for stainless steel. The key difference is that electropolishing also removes surface metal and improves Ra, while chemical passivation only modifies the existing surface without altering geometry or finish.
What surface finish specification should parts have before electropolishing?
Parts should arrive with a machined or ground finish no rougher than Ra 1.6 µm (63 µin) for best results. Electropolishing reduces Ra by up to 50%, so a coarser starting surface will still be coarser after treatment—the process amplifies existing finish quality rather than correcting poor machining. Deep tool marks, scratches, or pitting should be addressed mechanically before the part enters the electropolishing bath.
Conclusion
Electropolishing precision parts delivers three outcomes that mechanical finishing cannot match in a single step: a measurable Ra improvement, predictable and uniform material removal, and a passive surface layer that resists corrosion and contamination. Those properties matter most in medical, aerospace, and electronics applications where surface integrity directly affects part performance and regulatory compliance.
Two actions are worth taking now. First, confirm your pre-polish Ra and dimensional tolerances account for the 5–25 µm removal typical of a standard cycle. Second, verify that your manufacturing partner holds ISO 13485 certification if your parts enter a regulated supply chain—not every shop does. GC INDUS combines CNC machining, surface treatment, and full inspection protocols under one roof, so you can request a quote with your STEP file and get a finishing plan built around your tolerance stack from the start.
Recommended Articles
Explore more from our content library:


