
Book Appointment Now
How Orthogonal Machining Precision Boosts Tool Performance
Orthogonal machining precision refers to the accuracy and surface quality achieved when a cutting tool engages a workpiece along a single, well-defined cutting edge...
Orthogonal machining precision refers to the accuracy and surface quality achieved when a cutting tool engages a workpiece along a single, well-defined cutting edge perpendicular to the direction of cut, eliminating the side-cutting geometry present in oblique cutting. This two-dimensional cutting model isolates the key variables governing chip formation, cutting forces, and surface finish, making it the foundation for understanding and controlling precision in metal removal. Engineers use it to predict tool wear, optimize rake angles, and validate machining parameters before committing to full production runs.
What Is Orthogonal Machining Precision and How Does It Differ from Oblique Cutting?
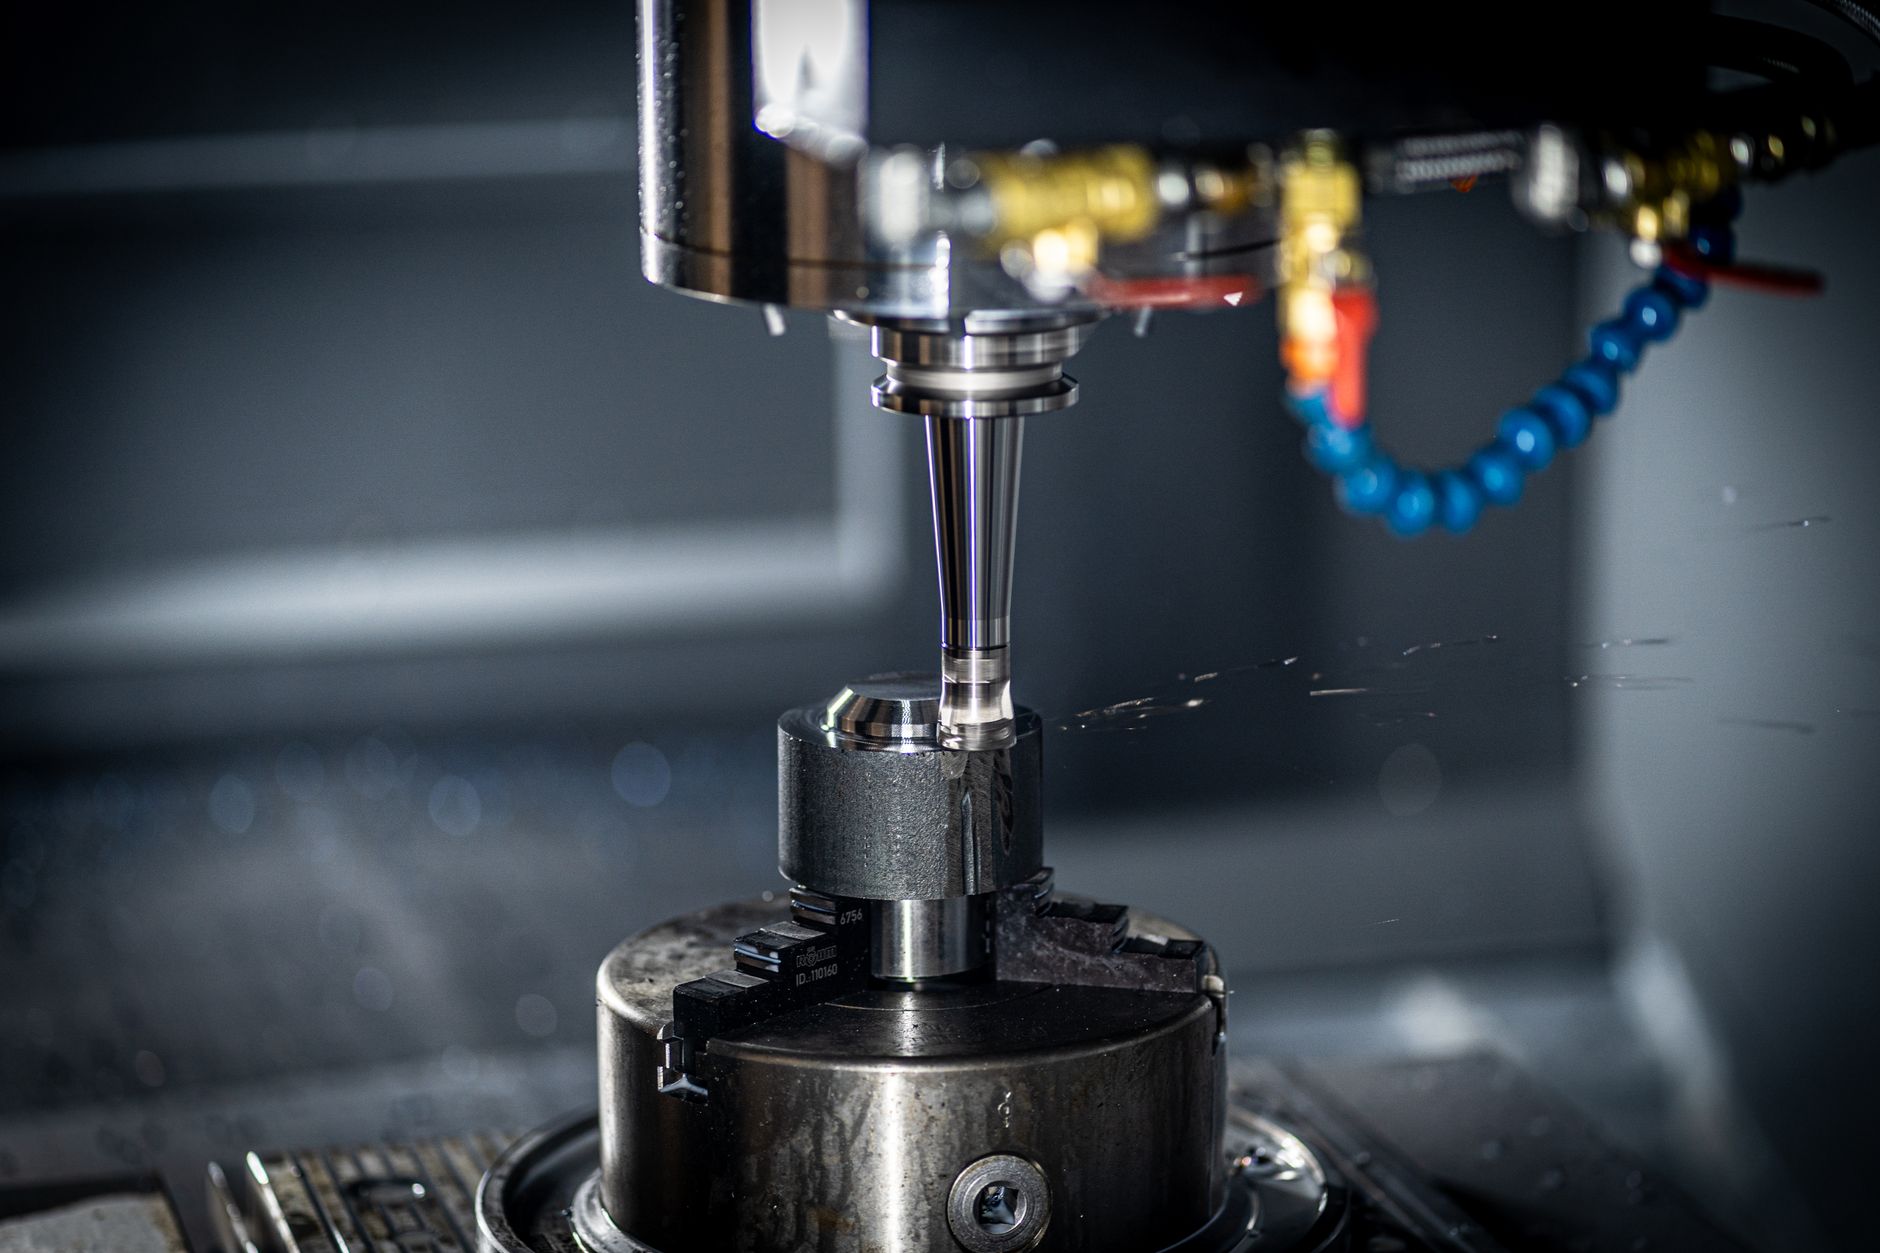
Orthogonal machining precision is achieved when the cutting edge sits exactly perpendicular to the cutting velocity vector, confining all chip flow to a single plane.
That geometric constraint is what makes the model useful. With chip formation locked to two dimensions, engineers can measure cutting forces, heat generation, and deformation without untangling the compound force vectors that appear in three-dimensional cutting. The result is a tractable model, one that forms the analytical backbone of precision machining research and process validation.
What Is the Chip Thickness Ratio and Why Does It Matter?
The chip thickness ratio, also called the cutting ratio, is the uncut chip thickness divided by the actual chip thickness after the cut. A ratio close to 1.0 means the chip is leaving the workpiece with minimal compression, which signals clean, predictable shear. A low ratio signals heavy deformation, which correlates with torn surfaces, improved cutting temperatures, and unpredictable tool wear.
Monitoring this ratio gives process engineers a direct, measurable indicator of whether a given combination of rake angle, feed rate, and workpiece material is producing controlled chip formation or fighting it. In precision work, where surface error budgets are measured in microns, that distinction is not academic.
Orthogonal vs Oblique Cutting: Force, Surface Finish, and Tool Life Compared
Oblique cutting introduces a third force component the moment the cutting edge tilts away from perpendicular. That side force drives chip flow across the rake face at an angle, accelerating flank wear unevenly and making surface finish harder to predict from one pass to the next.
The table below maps the three key differences between the two geometries.
| Factor | Orthogonal Cutting | Oblique Cutting |
|---|---|---|
| Force distribution | Two components (thrust and cutting force), fully measurable in a single plane | Three components, side force adds load variability and complicates force modeling |
| Surface finish predictability | High, fewer force vectors mean fewer vibration modes and less chatter-induced error | Lower, lateral chip flow creates micro-irregularities that vary with tool inclination angle |
| Tool life | More uniform flank wear, easier to model and predict | Uneven flank wear due to the side force component; tool life curves are harder to generalize |
Orthogonal geometry is physically realized in parting-off operations, broaching, and controlled laboratory turning set-ups where the tool width is narrower than the workpiece. These contexts are exactly why orthogonal cutting serves as the reference model for precision machining research, the geometry is clean enough to isolate individual variables. When GC INDUS engineers validate new cutting parameters before a production run, the same two-dimensional force logic underpins how they interpret tool wear data and surface roughness measurements.
Key Parameters That Govern Orthogonal Machining Precision
Rake angle, cutting speed, feed rate, and tool edge geometry are the four controllable variables that most directly determine dimensional accuracy and surface finish in orthogonal cutting.
Rake Angle in Orthogonal Cutting: Impact on Precision
A positive rake angle thins the shear zone and reduces friction at the rake face, which lowers cutting force and heat generation. Less heat means less thermal expansion of the workpiece during the cut, a direct benefit to dimensional repeatability. A negative rake angle strengthens the cutting edge and suits hard or abrasive materials, but it drives higher cutting forces and temperatures. Selecting the wrong rake angle for a given material degrades surface finish and introduces systematic dimensional error across a batch.
Cutting speed governs whether a built-up edge (BUE) forms on the tool face. Below a material-specific speed threshold, workpiece material welds to the rake face, then periodically fractures and smears across the machined surface, destroying surface precision and shifting the effective tool geometry unpredictably. Exceeding that threshold keeps the rake face clear and stabilizes the cut.
Feed rate sets the uncut chip thickness directly. A higher feed rate scales cutting force and increases elastic springback in the workpiece after the tool passes. On thin-walled or low-rigidity parts, that springback translates into measurable dimensional error, a mechanism that makes feed rate one of the most consequential parameters for orthogonal machining precision on flexible workpieces.
Tool edge sharpness determines whether the tool cuts or ploughs. When the edge radius is large relative to the uncut chip thickness, the tool ploughs rather than shears, generating subsurface residual stress that causes the part to distort dimensionally after unclamping.
Setup and Calibration Procedures for Orthogonal Machining Experiments
A disciplined setup sequence is essential before collecting any force or surface data. Follow these steps in order:
- Align the tool perpendicular to the feed direction. Any angular offset introduces an oblique cutting component that invalidates the plane-strain assumption the orthogonal model depends on.
- Mount the dynamometer to capture cutting force (Fc) and thrust force (Ft) independently. A two-component piezoelectric dynamometer mounted rigidly to the machine table prevents cross-talk between force channels.
- Fix the workpiece to eliminate compliance. Clamp directly over the cutting zone where possible; unsupported overhangs introduce vibration that corrupts both force signals and surface measurements.
- Run a baseline cut at conservative parameters. Measure chip thickness ratio and compare against the theoretical shear angle, agreement confirms plane-strain conditions and validates the experimental setup before full testing begins.

How Material Properties Shape Orthogonal Machining Precision
Workpiece material determines chip formation mode, cutting force magnitude, and the thermal load the tool-workpiece interface must absorb, all of which set the ceiling on achievable dimensional accuracy.
Aluminum vs Steel vs Composites: Material-Specific Precision Considerations
Aluminum alloys conduct heat well, which keeps thermal expansion errors low during orthogonal cuts. The trade-off is low yield strength: at slow cutting speeds, aluminum tends to weld onto the tool rake face, forming built-up edge (BUE). BUE smears material across the finished surface and degrades dimensional repeatability. Increasing spindle speed breaks this adhesion cycle, but the optimal speed window is narrow and material-grade dependent, so parameter selection matters as much as machine capability. For more information, see Viticulture De Precision En Medoc Guide Complet.
Carbon and stainless steels work-harden rapidly inside the primary shear zone. As the shear-zone temperature rises, specific cutting energy increases, and the cutting forces transmitted to the workpiece grow with it. Any compliance in the machine structure, spindle bearings, fixturing, or the tool overhang, translates directly into dimensional error. Orthogonal machining precision in steel therefore demands a stiffer setup than aluminum of equivalent geometry. Diffusion wear also becomes active at improved temperatures, causing crater growth behind the cutting edge and a gradual shift in effective rake angle.
Carbon fibre and glass fibre composites (CFRP/GFRP) do not form continuous chips. Instead, the cut produces delamination and fibre pull-out, and the severity depends on the angle between the fibre orientation and the cutting direction. Fibres oriented perpendicular to the cut tend to fracture cleanly; fibres running parallel or at shallow angles tend to deflect and pull rather than shear. Rake angle selection becomes the primary control lever: a sharper (more positive) rake reduces the compressive load on the laminate and limits sub-surface damage. Abrasive wear dominates tool degradation in composites, hard fibres erode the cutting edge continuously, rounding it and increasing the effective edge radius, which in turn raises the ploughing force and worsens surface finish.
Each material class degrades tool geometry through a different mechanism: abrasion in composites rounds the edge progressively; diffusion in steel grows a crater that shifts the rake face geometry; adhesion in aluminum deposits smeared material that alters the effective cutting profile. Each route reduces precision, but each requires a different countermeasure, coating chemistry, cutting speed, or coolant strategy.
When precision is the primary requirement, machinability index and thermal softening behaviour should guide both material selection and the allowable cutting parameter window. A material that softens quickly with temperature, such as certain aluminum alloys, permits higher speeds without thermal expansion penalty. A material with a high work-hardening rate demands conservative depth-of-cut and feed to keep cutting forces within the stiffness budget of the machine. GC INDUS applies this material-parameter logic across CNC milling, turning, and 5-axis operations, holding tolerances to ±0.001mm by matching cutting conditions to the specific mechanical and thermal profile of each workpiece material.
Software Tools and Simulation Platforms for Analyzing Orthogonal Machining Performance
FEA-based cutting simulation and CAM-integrated force models let engineers predict orthogonal machining precision outcomes—chip shape, cutting forces, and dimensional error—before a single part is cut.
CAM and FEA Platforms That Support Orthogonal Machining Simulation
Finite element analysis platforms model the orthogonal cutting zone by discretizing the workpiece and tool into a mesh, then solving for stress, strain, and heat at each node. The outputs—shear-plane angle, chip morphology, cutting force components Fc (primary) and Ft (thrust), and temperature distribution across the tool-chip interface—are verified against dynamometer measurements. Matching simulated forces to measured forces is the standard validation workflow before trusting a model for process design.
Three mesh formulations handle the physics differently. Lagrangian meshes move with the material, capturing chip separation and fracture accurately but at high computational cost. Eulerian meshes fix the reference frame to space, which speeds up steady-state flow calculations but struggles to model chip initiation. Arbitrary Lagrangian-Eulerian (ALE) formulations blend both: the mesh moves independently of the material, reducing distortion at the tool-chip contact zone while keeping computational cost manageable. ALE is now the most common choice for orthogonal cutting models where contact accuracy matters.
CAM environments use orthogonal cutting force models as direct inputs to chatter stability lobe diagrams. By mapping predicted force magnitudes against spindle speed and axial depth of cut, the software identifies speed ranges where the tool-workpiece system avoids resonance. Engineers select a stable spindle speed from the lobe diagram before the first cut—eliminating the trial-and-error passes that waste material and time.
How Simulation Tools Predict Precision Outcomes Before Physical Machining
Simulated cutting forces feed directly into elastic deflection calculations for the tool-workpiece system. A predicted Fc of, say, 80 N on a slender tool produces a calculable deflection that maps to a specific dimensional error at the part surface. Engineers iterate rake angle and feed rate in the model until predicted deflection falls within the target tolerance—at GC INDUS, that target can be as tight as ±0.001mm—before committing to a physical setup.
The largest source of simulation error is the material constitutive model, not the FEA solver itself. Johnson-Cook parameters—which describe how a material’s flow stress changes with strain, strain rate, and temperature—must be calibrated for each alloy and heat treatment condition. Published parameter sets often produce force predictions that diverge from measured values by 15–30% for less-common alloys. Physical orthogonal cutting experiments, using controlled rake angles and measured force outputs, remain the standard method for calibrating these parameters. Simulation accelerates development; physical cutting experiments keep the models honest.
How Manufacturers Can Implement Orthogonal Machining to Improve Precision and Reduce Costs
Orthogonal machining precision improves most when manufacturers follow a defined setup sequence, select tooling matched to the material, and monitor cutting forces continuously to catch tool wear before it produces scrap.
Practical Steps for Setting Up and Optimizing Orthogonal Machining in Production
1. Match tool geometry to material machinability. Start by selecting a rake angle and edge preparation suited to the workpiece. Aluminum alloys tolerate high positive rake angles; hardened steels demand tighter edge radii and harder substrates such as carbide or CBN. Getting this wrong shifts the cutting regime before the first chip forms.
2. Set cutting speed above the built-up edge threshold. BUE forms at low speeds and deposits material on the cutting edge, destroying dimensional consistency. Establish a speed that keeps the contact zone above the BUE transition for the specific material-tool pairing.
3. Set feed rate so uncut chip thickness exceeds the edge radius. When chip thickness falls below the edge radius, the tool ploughs rather than cuts. Ploughing induces subsurface damage and part rejection—a cost that far outweighs the upfront premium of tight-tolerance carbide or CBN tooling with controlled edge geometry.
4. Verify tool-edge orthogonality with a dial indicator. Confirm the cutting edge is perpendicular to the feed direction before committing to a batch. A misaligned edge introduces an oblique cutting component that invalidates the force predictions orthogonal theory provides.
5. Run a qualification cut before batch production. Measure surface roughness and dimensional deviation on the first part. This single step catches parameter errors before they propagate across a full run and trigger rework.
Cost reduction follows from process predictability. Orthogonal geometry produces consistent cutting forces, which reduces unexpected tool breakage—a primary driver of unplanned downtime. Consistent chip formation also prevents chip re-cutting, where loose chips re-enter the cut zone and scratch finished surfaces. Both failure modes generate rework; both are largely avoidable with controlled orthogonal parameters.
Monitor forces in-process to sustain precision over time. A dynamometer or spindle-load proxy tracks cutting force continuously. As the edge rounds with wear, force rises measurably before part dimensions degrade. That signal triggers a planned tool change at the right moment—not after a rejected part confirms the edge has failed.
Apply these principles beyond the lab. Parting, grooving, broaching, and face-turning operations all approximate orthogonal geometry in production. Applying orthogonal cutting theory to parameter selection in these operations—particularly speed, feed, and edge radius—directly improves first-pass yield on tight-tolerance features without requiring new equipment. GC INDUS applies this parameter discipline across CNC turning and milling operations, holding tolerances to ±0.001mm on production runs from a single prototype piece through high-volume batches.

Frequently Asked Questions
What is the shear plane angle in orthogonal cutting and how does it affect precision?
The shear plane angle is the angle at which the workpiece material shears as the cutting tool advances, and it directly controls chip thickness, cutting forces, and dimensional accuracy. A higher shear plane angle produces thinner chips and lower cutting forces, which reduces tool deflection and improves dimensional repeatability. Engineers use rake angle and cutting speed adjustments to influence this angle. When the shear plane angle is poorly controlled, force spikes cause micro-displacement at the tool tip, translating directly into out-of-tolerance features.
How does cutting speed affect surface finish in orthogonal machining?
Higher cutting speeds generally improve surface finish by reducing the built-up edge that forms on the tool face at low speeds. Built-up edge deposits material irregularly on the machined surface, creating roughness that defeats tight tolerance targets. Beyond a material-specific threshold, however, thermal softening can destabilize the cut. For most steel and aluminum alloys, operating in the mid-to-high speed range, matched to the tool coating and coolant strategy, produces the most consistent surface quality.
Can orthogonal machining principles be applied to CNC multi-axis operations?
Yes, orthogonal cutting theory provides the analytical foundation for multi-axis CNC programming, even though real cuts are rarely perfectly two-dimensional. Engineers use orthogonal models to predict chip load, cutting force direction, and heat generation at each tool engagement point, then apply those predictions when setting feeds, speeds, and tool paths on 5-axis machines. GC INDUS applies this approach across its 5-axis CNC and Swiss lathe operations to maintain tolerances as tight as ±0.001mm on complex geometries.
What causes dimensional error in orthogonal cutting and how can it be minimized?
Dimensional error in orthogonal cutting originates from three main sources: tool deflection under cutting force, thermal expansion of the workpiece, and tool wear that shifts the effective cutting edge position. Minimizing error requires controlling all three simultaneously, using rigid tooling setups to limit deflection, applying coolant to manage heat, and scheduling tool changes before wear reaches a threshold that shifts dimensions. In-process gauging and post-process inspection close the loop, catching drift before it produces scrap.
Conclusion
Orthogonal machining precision is not a single variable, it is the product of shear plane geometry, cutting force control, thermal management, and tool condition working together. Three actions matter most: set cutting parameters around the shear plane angle your material and tool geometry actually support; monitor tool wear proactively rather than reacting to scrap; and verify results with in-process gauging rather than end-of-run inspection alone.
If your current supplier cannot explain how they control these variables on your specific part geometry, request a process capability report, specifically Cpk values for the critical dimensions on your drawing, before committing to a production run.
Recommended Articles
Explore more from our content library:


