
Book Appointment Now
What Runout Compensation Is and Why It Boosts CNC Accuracy
Runout compensation in CNC machining corrects the small but measurable deviation between a tool's rotational axis and the spindle's true centerline, directly improving...
Understanding runout compensation CNC accuracy is essential. Runout compensation in CNC machining corrects the small but measurable deviation between a tool’s rotational axis and the spindle’s true centerline, directly improving dimensional accuracy and surface finish. Unmanaged runout causes diameter errors, chatter, and premature tool wear, all of which push finished parts outside tolerance. Compensation is applied through software offsets, precision toolholding, or a combination of both, and is essential whenever tight tolerances demand consistent, repeatable cuts.
What Runout Compensation Means for CNC Accuracy: runout compensation CNC accuracy
Runout is the measurable offset between a tool’s actual rotation path and the spindle centerline, and correcting it is the basis of runout compensation CNC accuracy work depends on.
The formal measurement is Total Indicator Runout (TIR), recorded in microns or thousandths of an inch using a dial test indicator held against the rotating tool or holder. TIR captures the full deviation across one complete spindle revolution.
Radial vs. Axial Runout: Which Affects Your Parts More
Radial runout describes eccentricity perpendicular to the spindle axis, the tool wobbles side to side as it rotates. This directly widens the effective cutting diameter, producing bores that are oversize and outside walls that are undersize relative to the programmed path.
Axial runout describes deviation along the spindle axis, the tool oscillates forward and backward with each revolution. This matters most in facing operations and drilling, where it creates uneven step depths and inconsistent surface finish on flat features.
In practice, radial runout causes more dimensional damage on turned and milled diameters. Axial runout becomes the dominant problem in deep drilling and thread milling, where depth consistency is critical.
How Runout Accumulates Through the Spindle-Holder-Tool Stack
Runout is not a single-source error, it compounds at every interface in the spindle-holder-tool assembly. The spindle taper contributes its own TIR, the toolholder adds another increment, and the tool itself introduces a third. Each value stacks, so the total runout at the cutting edge can be several times larger than any individual component measurement.
With multiple cutting edges in play, the effect multiplies further. One flute cuts deeper than the others, carrying a disproportionate chip load. That uneven load accelerates wear on the engaged flute, shifts the effective cut diameter, and produces surface irregularities, all before the part has moved to its next feature.
Compensation does not eliminate this stacking. It applies a corrective offset, in the CNC control, in the toolholder design, or in both, so the programmed cutting path matches the tool’s actual behavior. The tighter the tolerance band, the less accumulated runout the process can absorb. At ±0.001mm tolerances, even a few microns of uncompensated TIR can push a finished part outside specification.
How to Measure Runout Before Applying Compensation
Accurate runout measurement requires a dial test indicator, a magnetic base, and a precision reference surface, without all three, your readings are unreliable.
Measuring before you compensate is the step most machinists skip or rush. Any runout compensation CNC accuracy strategy built on a bad baseline reading will introduce error rather than remove it.
Setting Up the Dial Indicator for Repeatable Readings
You need three instruments working together. A dial test indicator (DTI) or electronic runout gauge gives you the actual displacement reading. A magnetic base holds the indicator rigid against the machine table or spindle housing, any flex in the base creates false readings. A precision reference surface, such as a granite plate or a certified ground flat, gives you a stable datum to zero against.
The setup procedure follows a fixed sequence. First, mount the indicator tip against the tool shank or collet nose at a 90-degree contact angle. Second, rotate the spindle by hand through a full 360-degree revolution, never use power rotation at this stage. Third, record the full Total Indicator Reading (TIR): the difference between the highest and lowest values the gauge sweeps through. That single TIR figure is what you are compensating for.
Repeat the measurement at least three times and average the results. A single pass can be skewed by surface contamination or an inconsistent contact point.
Identifying Whether Runout Originates at the Spindle, Holder, or Tool
The compensation method you choose depends entirely on where in the tooling stack the error lives. Measure at three points in sequence: the spindle taper alone, then the holder installed, then the tool installed. If the reading jumps significantly at the holder stage, the holder seat is damaged or contaminated. If it jumps at the tool stage, the shank is out-of-round or the collet is worn.
Spindle bearing wear produces a consistent, repeating runout pattern across all tools. Collet contamination, chips, coolant residue, or burrs, produces variable readings that change between tool changes. Isolating the source before applying any offset prevents you from masking a mechanical problem that will worsen over time.
Measure at every tool change, at the start of each new job setup, and immediately after any crash or extended thermal soak. Baseline readings recorded over time also tell you when compensation values have drifted far enough to require recalibration rather than a simple offset adjustment.
Software vs. Hardware Runout Compensation: Comparing Both Approaches
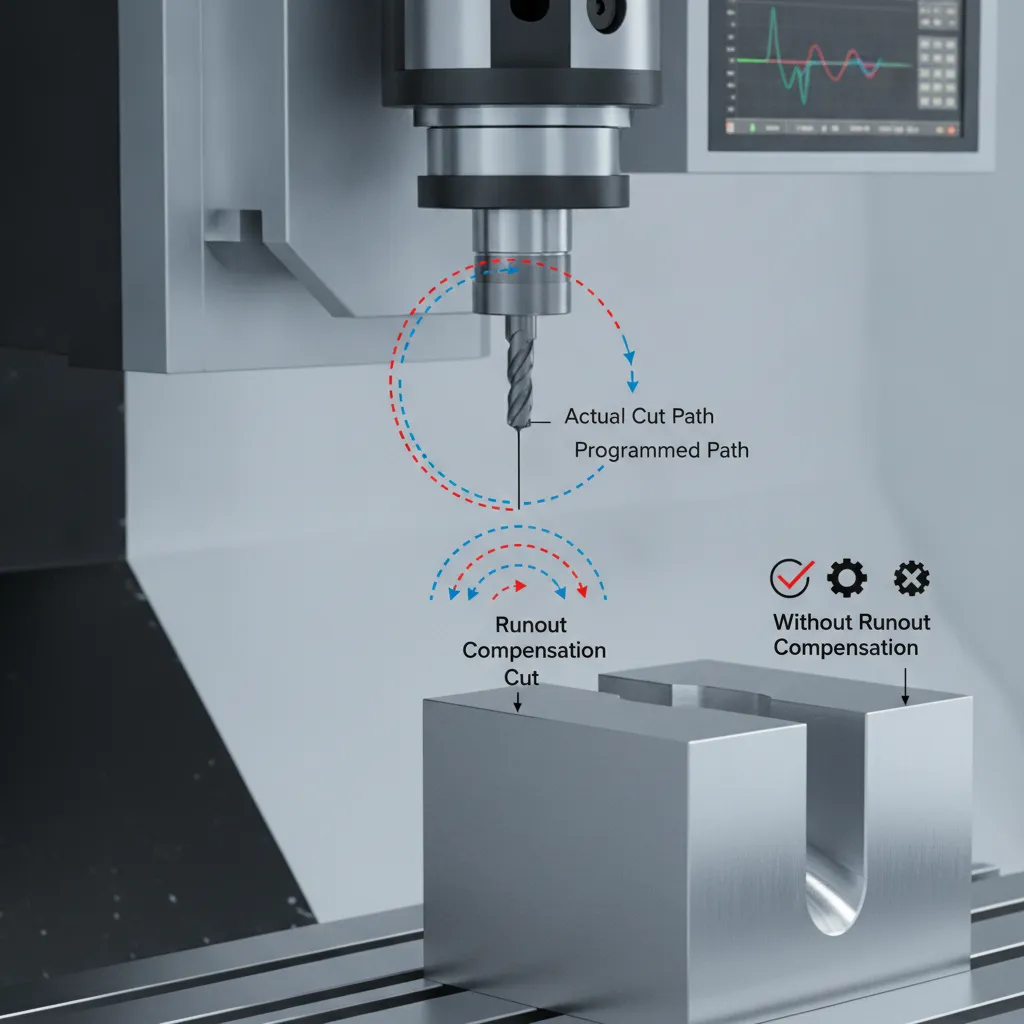
Software and hardware runout compensation each solve a different part of the problem, one corrects for eccentricity in the tool path; the other eliminates it at the source.
Modern CNC controls accept a measured runout value and apply a dynamic tool-center-point (TCP) offset or cutter radius correction, shifting the programmed path by the known eccentricity. This approach works well for finishing passes, where spindle speeds are controlled and the runout value is stable. The limitation appears during high-speed roughing: at improved RPM, thermal growth and vibration cause runout to drift, and a static software offset cannot adapt to that change in real time.
When Software Offsets Reach Their Limits
Software compensation assumes the error it corrects is fixed. When runout compensation CNC accuracy depends on a thermally stable setup, that assumption holds. When the spindle heats up over a long roughing cycle, the eccentricity shifts, and the pre-measured offset now corrects for a value that no longer exists, potentially introducing error rather than removing it.
High-speed roughing also generates cutting forces that flex the tool and holder, adding a dynamic component to runout that a static TCP offset cannot account for. Software compensation is most reliable when paired with hardware that has already reduced runout to a small, stable residual.
Precision Toolholding Options and How They Reduce Eccentricity at the Source
Hardware solutions attack runout before the spindle turns. Shrink-fit holders heat the bore to expand it, insert the tool shank, then cool to create an interference fit with near-zero radial play. Hydraulic chucks use pressurized fluid to apply uniform radial clamping force around the shank, centering it mechanically. Balanced collet systems, precision-ground collets matched to specific shank diameters, reduce the asymmetric mass distribution that amplifies eccentricity at high RPM.
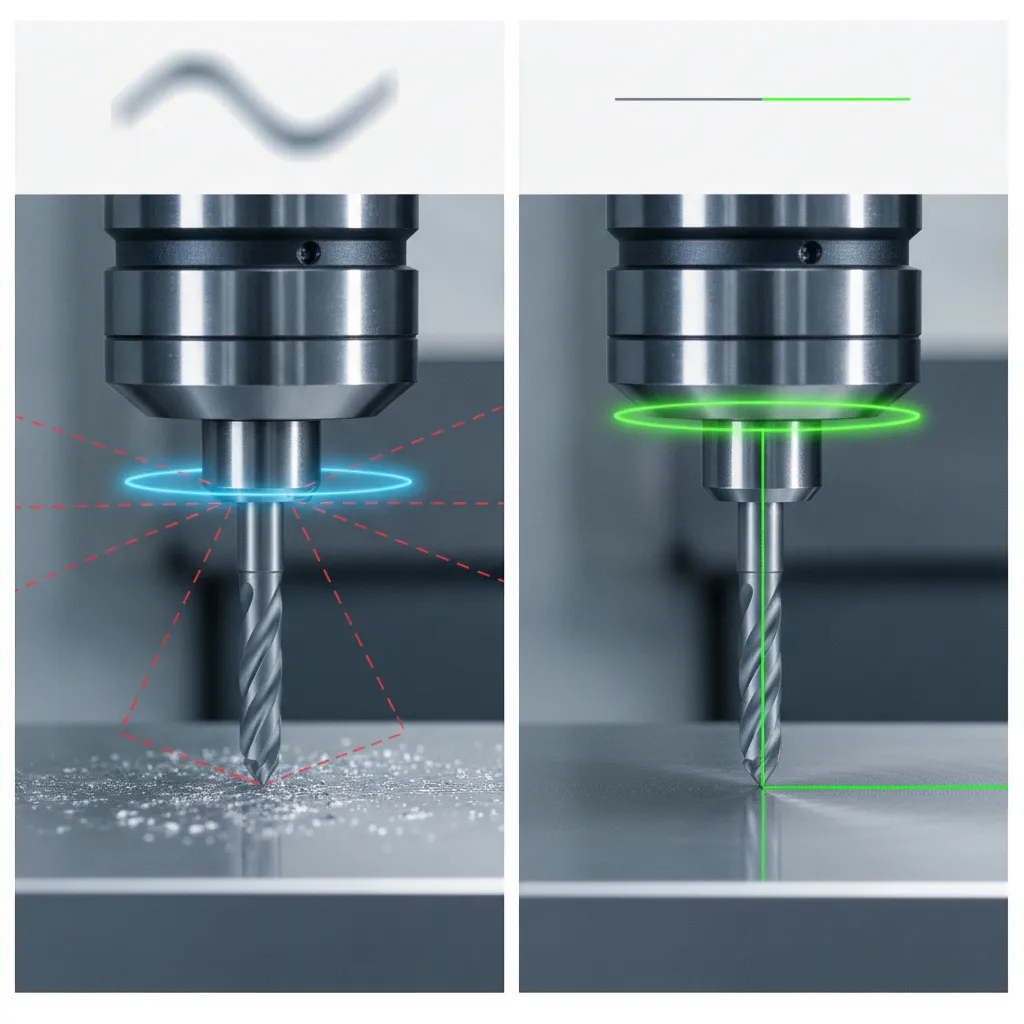
Each mechanism reduces eccentricity at the source rather than correcting for it downstream, which is a qualitatively different outcome: the error is smaller to begin with, not masked by an offset.
The strongest approach combines both methods. Hardware minimizes residual runout to a small, stable value; software offsets the remainder. This layered strategy is standard practice in aerospace and medical part production, exactly the environments where GC INDUS holds tolerances to ±0.001mm across CNC milling, 5-axis, and Swiss lathe operations under ISO 9001 and ISO 13485 quality protocols.
Troubleshooting Runout Compensation Failures and Knowing Its Limits
Runout compensation fails when the error it corrects is no longer the error the machine is producing, three failure modes account for most of these breakdowns.
The Three Most Common Failure Modes
Thermal growth is the leading culprit. A compensation offset set on a cold spindle becomes inaccurate once the machine reaches operating temperature, because the spindle housing and toolholder expand at different rates, shifting the runout value away from what was measured.
Collet contamination is the second mode. A single chip or a film of corrosion on the collet bore or tool shank reintroduces eccentricity between the measurement cycle and the cut. The offset in the control is correct, the physical setup is not.
Software offset drift is the third. When an operator changes a tool without updating the control’s tool table, the active offset no longer matches the current tool’s runout. The control compensates for a tool that is no longer in the spindle.
Thermal Drift and Why Compensation Set Cold Fails at Temperature
The diagnostic sequence starts at operating temperature, not at startup. Re-measure runout after the spindle has run for at least 20 minutes under normal load, this is the condition the offset must match. Next, inspect the collet bore and tool shank under magnification for chips or surface corrosion, either of which shifts the contact geometry. Finally, pull up the control’s active offset and confirm it matches the last recorded measurement; a mismatch here explains most cases of runout compensation CNC accuracy failures that appear without any obvious mechanical change.
When Spindle Bearing Condition Makes Compensation Unreliable
Worn spindle bearings produce runout that changes with spindle speed and cutting load, it is not a fixed value. No static offset can track a moving target. When repeated measurements at the same conditions return different runout values, compensation is masking a symptom rather than correcting a defined error.
The decision to keep compensating or investigate the mechanical root cause rests on one question: is the runout value stable? A stable, repeatable value, even a relatively large one, can be offset reliably. A value that shifts between measurements, or that changes across the speed range, signals bearing wear or toolholder damage that requires inspection and likely component replacement. Chasing a variable error with a fixed offset does not improve part quality; it introduces unpredictable deviation.
Applying Runout Compensation in Practice: Best Practices for Consistent CNC Accuracy
Runout compensation delivers consistent CNC accuracy only when it follows a repeatable, documented sequence, not when applied as a reactive fix after parts fail inspection.
The Setup Sequence That Prevents Drift
Start every setup by cleaning and visually inspecting the toolholder and collet for chips, wear, or fretting on the taper. Contamination as thin as a metal shaving can introduce measurable runout before the spindle turns once.
After tool installation, measure runout at the tool tip with a dial test indicator or non-contact probe. Enter or verify the compensation offset in the control before the first cut, then record the reading against the job traveler. That paper trail lets you compare readings across setups and catch gradual holder wear before it affects part dimensions.
Toolholding selection belongs at the quoting or process-planning stage, not on the shop floor at setup time. Specifying shrink-fit or hydraulic holders for tight-tolerance bores and turned diameters reduces the compensation burden before the machine starts cutting. Standard ER collets remain appropriate for roughing passes where runout tolerance is wider, choosing the right holder type upfront is the most cost-effective form of runout management available.
Building Runout Checks Into First-Article and In-Process Inspection
Tie compensation verification to three defined checkpoints: first-article inspection, scheduled in-process gauging intervals, and any event that could disturb the tool stack, a crash, a programmed tool change, or a spindle warm-up cycle after a cold start. Each of these events can shift runout by several microns, enough to push a tight-tolerance feature outside specification.
When runout compensation CNC accuracy checks are embedded in the quality plan rather than left to operator judgment, the results are measurable: stable diameter control, predictable surface finish, and lower scrap rates across the production run. At GC INDUS, full inspection protocols, including dimensional verification against job travelers, are standard practice on every order, which is how we hold tolerances to ±0.001mm across CNC milling, turning, and 5-axis operations. The time invested in a disciplined compensation workflow pays back directly in fewer rejected parts and less rework at final inspection.
Frequently Asked Questions
How often should runout be measured and compensated on a CNC machine?
Measure runout at the start of every new job, after any tool change, and after any spindle crash or unexpected load event. Thermal growth during a long production run can shift readings, so re-checking mid-cycle is good practice on tight-tolerance work. For high-volume production with stable tooling, a scheduled check every shift is a reasonable baseline, but any change in surface finish or dimensional drift is a signal to measure immediately.
Can runout compensation fully replace the need for a precision toolholder?
No, compensation corrects for measured error but cannot substitute for a quality toolholder that minimizes error at the source. Software offsets and adjustable toolholders reduce the effect of runout; they do not eliminate the mechanical instability, uneven cutting forces, or accelerated tool wear that a worn or low-grade holder causes. Treat compensation as a fine-tuning layer on top of sound toolholding practice, not a workaround for poor equipment.
Does spindle speed affect runout, and does compensation need to change at different RPMs?
Yes, spindle speed directly affects runout because centrifugal forces and bearing dynamics change as RPM increases. A toolholder that measures 3 µm of runout at 5,000 RPM may read significantly higher at 20,000 RPM due to imbalance-driven deflection. If your process runs across a wide speed range, measure runout at the actual operating RPM rather than at a static or low-speed setting, and apply compensation values specific to each speed condition.
What level of runout is acceptable before compensation becomes necessary for tight-tolerance parts?
For parts held to tolerances of ±0.01 mm or tighter, runout above 5 µm (0.005 mm) warrants active compensation. As a general rule, total runout should stay below 10–15% of the part tolerance to avoid consuming the entire tolerance budget on a single error source. Parts targeting ±0.001 mm, the kind GC INDUS holds routinely, require runout control well under 2 µm before compensation offsets are applied.
Conclusion
Runout compensation is not a single fix, it is a discipline that combines accurate measurement, appropriate toolholding, offset management, and process verification. The clearest takeaway: measure runout at operating RPM, not at rest, because the two readings can differ enough to invalidate your offsets entirely. Second, compensation works best when it fine-tunes an already-controlled setup, not when it papers over worn holders or poorly maintained spindles.
If your parts are held to tolerances tighter than ±0.01 mm, start by auditing your current runout readings against your tolerance budget. For components where that margin is ±0.001 mm, request a quote from GC INDUS and share your STEP file, the engineering team can identify where runout risk sits in your specific geometry before production begins.
Recommended Articles
Explore more from our content library:


