
Book Appointment Now
How Runout Affects CNC Machining Quality of Finished Parts
Runout in CNC machining is the deviation of a rotating tool or workpiece from its true axis of rotation — and it directly determines whether finished parts meet tolerance....
Understanding runout CNC machining quality is essential. Runout in CNC machining is the deviation of a rotating tool or workpiece from its true axis of rotation, and it directly determines whether finished parts meet tolerance. Even small amounts of runout cause dimensional errors, poor surface finish, accelerated tool wear, and improved scrap rates. Managing runout is not optional in precision work: it is the difference between parts that pass inspection and parts that don’t.
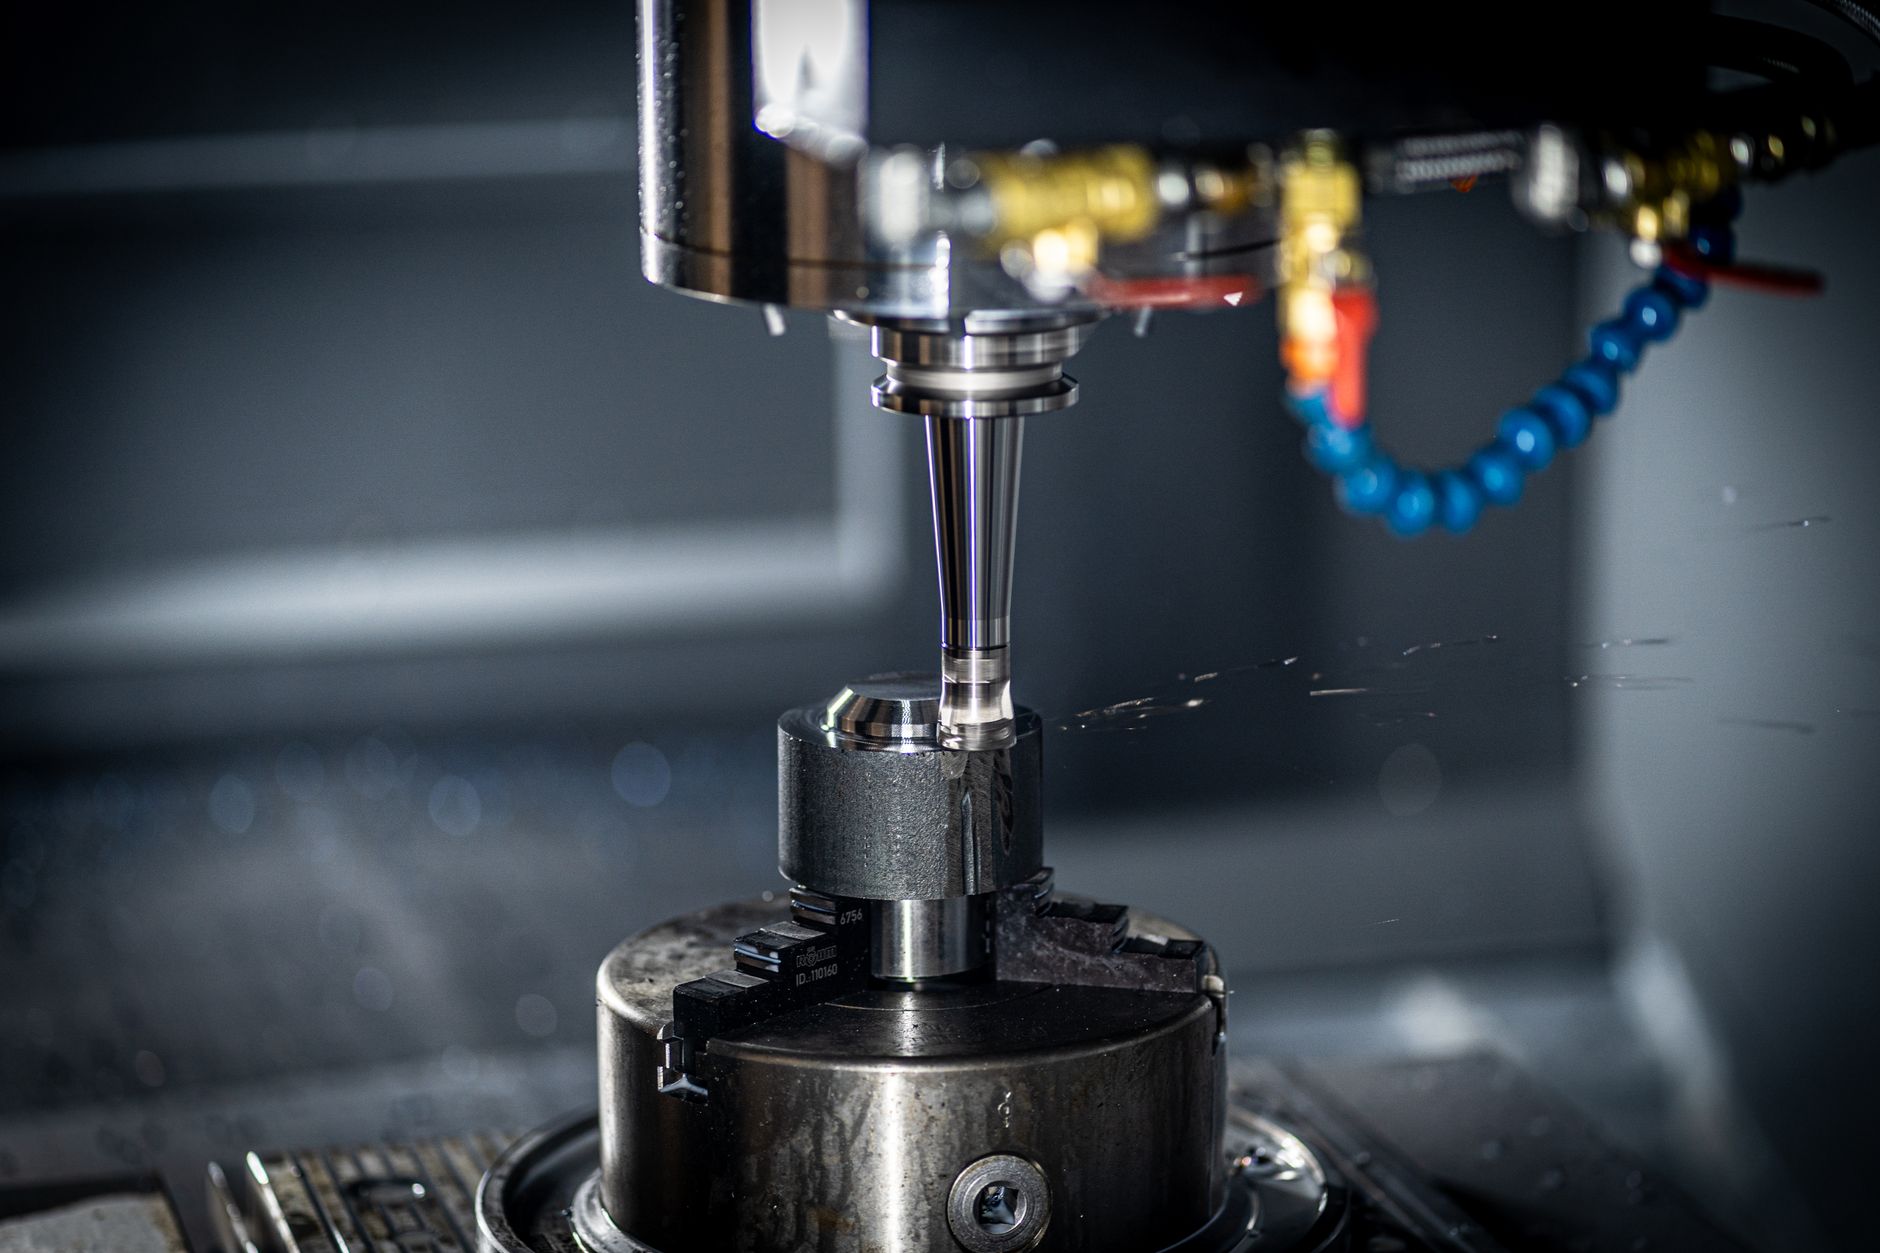
What Runout in CNC Machining Quality Actually Means: runout CNC machining quality
Runout is a rotational error, the measurable distance a spinning tool or workpiece deviates from its true geometric axis during a cut.
Two distinct types exist, and each corrupts different part features. Understanding both is the starting point for any serious discussion of runout CNC machining quality.
Radial vs. Axial Runout: Which Type Damages Your Parts
Radial runout is lateral deviation, the cutting edge sweeps a slightly larger or smaller circle than intended. The result shows up in bored hole diameters that measure out-of-round, turned diameters that vary along their length, and chatter marks across the surface where the tool alternately cuts too deep and too shallow.
Axial runout is end-to-end wobble along the spindle axis. It corrupts face flatness, produces inconsistent thread depths, and causes facing operations to leave a spiral rather than a flat surface. A part can pass a diameter check and still fail on face geometry because of axial error alone.
Engineers specify Total Indicator Runout (TIR) on engineering drawings to capture both effects in a single measurement. A dial indicator records the full range of deviation, maximum reading minus minimum reading, across one complete rotation. TIR differs from simple eccentricity because it accounts for every geometric imperfection contributing to that sweep, not just the offset of a center point. That completeness is why TIR is the standard convention on GD&T drawings rather than a simpler eccentricity callout.
The mechanical amplification effect makes TIR control urgent at every stage of the machine setup. A small spindle error does not stay small, it multiplies as it passes through the toolholder and reaches the cutting edge. The longer the tool overhang, the larger the error at the part surface relative to the original spindle deviation.
How Runout Tolerance Standards Differ Across Industries
Tolerance requirements tighten significantly as applications move from general manufacturing toward automotive and then aerospace, not arbitrarily, but because the consequences of failure change at each level.
In general manufacturing, a loose assembly stack-up absorbs small dimensional errors without functional impact. Automotive Tier-1 suppliers face tighter limits because components must assemble predictably across high production volumes; a bore that is slightly out-of-round in a fuel system or transmission housing causes premature wear that appears in the field, not on the production floor. Aerospace and medical applications add regulatory certification requirements on top of functional ones, a part that fails a CMM inspection cannot be reclassified or reworked without documented corrective action, making runout control a compliance issue, not just a dimensional one.
The cascade consequence is concrete: poor runout control produces out-of-round bores, inconsistent thread depths, surface chatter marks, and CMM failures, each of which triggers rework, delays, or scrap. Catching runout error at the spindle setup stage costs far less than catching it at final inspection.
What Causes Runout in CNC Machines and How to Measure It
Runout in CNC machining originates from worn or contaminated mechanical components, thermal growth during production, and procedural errors during tool setup.
Primary Mechanical Causes
Spindle bearing wear is the most common source of eccentricity. As bearing surfaces degrade, the spindle no longer rotates on a true centerline, the tool tip traces an elliptical path instead of a perfect circle, and every cut reflects that deviation.
Toolholder contamination introduces a separate problem. Chips, coolant residue, or microscopic burrs on the taper seat prevent full contact between the holder and spindle, shifting the tool axis off-center before the spindle even turns. Collet wear compounds this: a worn collet grips unevenly, allowing the tool shank to seat at a slight angle. Improper tool seating, not fully engaging the drawbar or failing to clean the taper, produces the same effect. On turning centers, chuck jaw wear causes the workpiece itself to run eccentric, which shifts the cutting relationship rather than the spindle.
Thermal growth is a secondary but significant driver of runout CNC machining quality problems. Spindle bearings generate heat during operation, and differential expansion between the spindle shaft and housing shifts the tool centerline by several microns over the first 20–30 minutes of a production run. Warm-up cycles, running the spindle at graduated speeds before cutting, reduce this drift. Machines with active thermal compensation use temperature sensors to apply real-time offsets that correct for the shift automatically.
Step-by-Step Runout Measurement Procedure for CNC Shops
Mount a dial test indicator (DTI) or electronic indicator on a magnetic base secured to the machine table or spindle housing. Position the indicator tip perpendicular to the rotating surface, either the toolholder body or a precision test bar seated in the spindle taper.
- Zero the indicator at the first contact point with light preload on the stylus.
- Rotate the spindle by hand through at least one full revolution, sampling readings at 90° intervals (0°, 90°, 180°, 270°).
- Record the maximum positive and maximum negative deflections from zero across the full sweep.
- Calculate TIR (Total Indicator Reading) by adding the absolute values of those two extremes, this single figure represents the full runout at that measurement point.
For tighter-tolerance work, laser alignment tools and air-bearing spindle analyzers provide higher resolution than a standard DTI. They capture continuous data across the full rotation rather than discrete sampled points, revealing lobing patterns and harmonic errors that a four-point DTI sweep can miss entirely. For more information, see Artisan Gelato Crafted With Quality And Care.
How to Calculate and Interpret Runout on Mills vs. Turning Centers
The reference datum changes depending on machine type, and using the wrong datum produces a measurement that doesn’t reflect actual cutting conditions.
On a machining center, measure runout at the spindle taper bore or at the toolholder gauge line, the point where the holder seats against the spindle face. This captures eccentricity introduced by the spindle and holder together. On a turning center, measure at the chuck jaw faces or between centers using a precision ground test bar. Here the workpiece is rotating, so the datum is the chuck centerline relative to the machine’s axis of rotation.
A reading below 0.005mm TIR is generally acceptable for general-purpose milling. Medical and aerospace features with tolerances at ±0.001mm, the level GC INDUS holds on precision CNC work, require runout well below that threshold, typically verified at both the gauge line and the tool tip to catch any angular error introduced by tool length.

How Runout Affects Production Costs, Scrap Rates, and Part Quality
Unmanaged runout in CNC machining quality control directly generates scrap, accelerates tool wear, and degrades surface finish, all without any change to programmed parameters.
How Runout Drives Scrap and Rework in High-Volume Production
The scrap mechanism starts at the cutting diameter. When a tool runs off-center, it traces a larger effective circle than its nominal diameter, shifting bored diameters and turned features outside their tolerance band. Parts can pass in-process gauging at the machine, then fail CMM inspection at final check because the runout error was never captured mid-cycle.
Tool consumption rises through the same mechanism. An off-center tool distributes chip load unevenly across its cutting edges, one edge takes a heavier cut while the opposite edge barely engages. That imbalance accelerates edge wear and micro-chipping without any change to programmed feeds or speeds, shortening tool life intervals and raising tooling cost per part.
Surface finish suffers in a specific way. The eccentric cutting path produces a lobed profile, visible as chatter marks or measurable out-of-round geometry. Sealing surfaces, bearing bores, and precision mating faces are particularly vulnerable: even a small lobe height can prevent a seal from seating correctly or cause a bearing to run with preload variation.
The damage compounds across multi-operation parts. A bore machined with excessive runout in operation one becomes a mislocated datum when the part is re-fixtured for operation two. Each subsequent operation inherits and amplifies the original error, a classic tolerance stack-up that can push a finished part out of specification even when every individual operation appeared in control.
Manufacturers who reduce runout at setup see a consistent pattern: tighter dimensional spread across a batch, fewer failures at final inspection, and more predictable tool change intervals. These are structural improvements, not marginal gains, they follow directly from giving each cutting edge a consistent, repeatable engagement with the workpiece.
Best Practices to Reduce Runout on Different CNC Machine Types
Reducing runout starts with toolholder selection, then machine-specific setup habits, and finally a consistent preventive maintenance schedule for spindle health.
Toolholder Selection: Which Types Deliver the Lowest Runout
Toolholder choice is the single highest-use intervention for runout CNC machining quality. Standard ER collet chucks require a small clearance gap between the collet and bore so the tool can be inserted, that gap is the primary source of eccentricity. Hydraulic holders eliminate it by using fluid pressure to grip the tool shank uniformly across its full circumference, with no clearance gap and no asymmetric clamping force. Shrink-fit holders achieve the same result thermally: the bore is heated to expand, the tool is inserted, and the bore contracts around the shank as it cools, producing a near-zero runout interference fit.
Both holder types consistently outperform ER collets in measured TIR at the tool tip, the mechanical reason is the same in each case: uniform, gap-free contact around the full shank diameter. For finish-critical or tight-tolerance work, hydraulic and shrink-fit holders are the default choice at GC INDUS, where we hold tolerances to ±0.001mm across CNC milling and turning operations.
Runout Reduction on 5-Axis Mills vs. Turning Centers
5-axis machining centers reposition the tool continuously through multi-axis moves. Any eccentricity at the spindle traces a larger error arc at the part surface as the tool tilts away from center, the longer the tool overhang, the greater that arc. Short, balanced tooling is not optional on 5-axis work; it is a geometric necessity. Balanced toolholders also reduce vibration at higher spindle speeds, which compounds the benefit.
Turning centers present different runout sources. Chuck jaw wear accumulates over time, so grinding jaws in-situ, on the machine itself, removes that accumulated error and restores true concentricity. For shafts requiring the tightest concentricity, between-centers turning bypasses the chuck entirely, referencing the part on its own centerline. Long workpieces add deflection as a runout contributor; steady rests support the workpiece mid-span and keep it on-axis under cutting load.
Preventive maintenance addresses runout causes before they appear in parts. Periodic bearing preload checks catch spindle wear early, a loose bearing allows the spindle to shift under load, which shows up as variable runout. Cleaning and inspecting the spindle taper before each tool change removes chips and fretting damage that prevent full toolholder seating. Balancing toolholders to the spindle’s operating speed range eliminates centrifugal eccentricity at high RPM.
At the operator level, three zero-cost habits make a measurable difference: clean both the taper and toolholder bore before every tool change, torque collet nuts to the manufacturer’s specification rather than by feel, and rotate the toolholder in the spindle to find the clocking position where measured TIR is lowest before locking it down. These steps cost nothing and consistently reduce setup-to-setup runout variation.
Tools and Procedures to Diagnose and Fix Runout Problems in Your Shop
Diagnosing runout requires a dial test indicator, a magnetic base, a precision test bar, and a structured three-point measurement sequence that isolates the error source.
Measurement Equipment Required to Identify Runout
Four instruments form the foundation of any shop-floor runout diagnostic. Each one plays a distinct role in tracing the error to its source.
- Dial test indicator (0.001mm or 0.0001-inch resolution): Detects the actual deviation as the spindle rotates. Resolution at this level is necessary to catch the small errors that directly affect runout CNC machining quality before they produce scrap.
- Magnetic base: Holds the indicator rigid against the machine column or table. Any flex in the base introduces measurement noise that masks the true runout value.
- Precision test bar or reference mandrel: Provides a known-true reference surface at the spindle taper and at the gauge line. It lets you separate spindle geometry errors from holder or tool errors.
- Surface plate (for off-machine checks): Allows you to inspect toolholder concentricity and collet condition away from the machine, confirming whether a worn holder is the culprit before reinstalling it.
The diagnostic sequence runs in three steps: measure at the spindle taper first, then at the toolholder gauge line, then at the tool tip. Each measurement narrows the error source, spindle, holder, or tool, so corrections target the actual problem rather than the symptom.
How to Verify Runout Improvements After Correction
Once you identify the error source, match the correction to it directly. A worn or contaminated toolholder gets re-seated or replaced. Worn collets get swapped, a collet that has cycled through thousands of tool changes loses its grip geometry and adds runout even when it looks intact. Chuck jaws that have drifted from repeated clamping loads get re-ground in place. Spindle preload that has relaxed over time gets adjusted according to the machine builder’s specification.
After each correction, re-measure at all three points in the diagnostic chain. Critically, take the final verification reading after a full spindle warm-up cycle, typically 10 to 20 minutes at operating speed. A cold spindle runs with different bearing clearances than a thermally stabilized one, and a cold-spindle measurement alone can produce a false pass that only reveals itself mid-production.
Document the post-correction readings as the new baseline for that machine and operation type. Set acceptance limits by machine and by process, a roughing operation tolerates more runout than a finish bore on a medical implant component. Feed those baselines into a preventive maintenance schedule with defined re-check intervals, so runout drift triggers a scheduled inspection rather than an unplanned stoppage. Shops that treat runout data as a living record, rather than a one-time check, catch bearing wear and holder degradation before they reach the part.

Frequently Asked Questions
What is the difference between runout and concentricity in CNC machining?
Runout measures how much a rotating feature deviates from its true axis during motion, while concentricity measures how well two circular features share the same center point. Runout is a dynamic measurement captured with a dial indicator while the part or tool spins. Concentricity is a static geometric tolerance defined in GD&T. In practice, excessive runout often signals a concentricity problem, but the two are distinct measurements requiring different inspection methods.
How often should CNC spindle runout be checked in a production environment?
Spindle runout should be checked at the start of each shift in high-volume or tight-tolerance production, and at minimum once per day in general machining. Thermal growth during warm-up affects readings, so measure after the spindle has run for 15–20 minutes. Any crash, tool pull-out, or sudden surface finish change should trigger an immediate check, regardless of schedule.
Can worn toolholders cause runout even on a well-maintained spindle?
Yes, a worn or contaminated toolholder is one of the most common sources of runout, even when the spindle itself measures within spec. Fretting wear on the taper interface, nicks on the flange face, and debris in the bore all introduce eccentricity between the spindle centerline and the cutting tool. Replacing or reconditioning toolholders is often the fastest fix when spindle runout checks out clean but part quality has degraded.
What level of runout is acceptable for general CNC machining versus precision aerospace work?
General CNC machining typically accepts total indicator runout (TIR) in the range of 0.01–0.05 mm, depending on feature tolerances. Precision aerospace and medical applications routinely demand TIR below 0.005 mm, and some bearing or turbine component work pushes below 0.002 mm. The acceptable threshold is always driven by the part’s functional tolerance stack, not by a universal standard, so engineers should work backward from the tightest feature tolerance on the drawing.
Conclusion
Runout is a compounding problem: a worn toolholder adds to spindle error, which adds to thermal drift, and the part at the end of the chain absorbs all of it. The engineers who control runout best treat it as a system, measuring at the spindle, the toolholder, and the workpiece fixture, not just one point in isolation.
Three actions make the biggest difference: establish a documented runout baseline for every spindle, replace toolholders on a scheduled cycle rather than waiting for failure, and specify TIR limits explicitly on drawings so inspection has a clear pass/fail criterion.
If your current supplier cannot tell you the measured TIR on your critical features, that is the right question to ask on your next RFQ, and a good reason to request a sample inspection report before committing to a production run. GC INDUS provides full inspection protocols and holds tolerances to ±0.001 mm; request a fast quote with your part drawing to see what that means for your specific application.
Recommended Articles
Explore more from our content library:
- <a href="https://gcindus.com/what-is-runout-compensation-in-cnc-machining-and-why-it/" title="What Runout Compensation Is and Why It Boosts CNC Accuracy”>What Runout Compensation Is and Why It Boosts CNC Accuracy
- Why Tolerance Stack-Up Matters in Multi-Part Manufacturing
- Optimizing Cutting Speed and Feed Rate for CNC Efficiency
- How Orthogonal Machining Precision Boosts Tool Performance
- How to Master Tapping and Threading in CNC Precision


