
Book Appointment Now
How to Master Tapping and Threading in CNC Precision
Learn how tapping threading CNC precision works, from tap types and methods to common failures, inspection, and when to choose thread milling instead.
Understanding tapping threading CNC precision is essential. Tapping and threading in CNC precision machining are the two primary methods for creating threaded holes in a part. Tapping uses a rotating cutting tool called a tap to cut internal threads directly into a pre-drilled hole, while threading (or thread milling) uses a multi-point cutter to interpolate the thread profile. The right choice depends on material, hole geometry, production volume, and required thread quality, each method carries distinct trade-offs in speed, tool cost, and reliability.
What Is Tapping and Threading in CNC Precision Machining, and How Do They Differ?
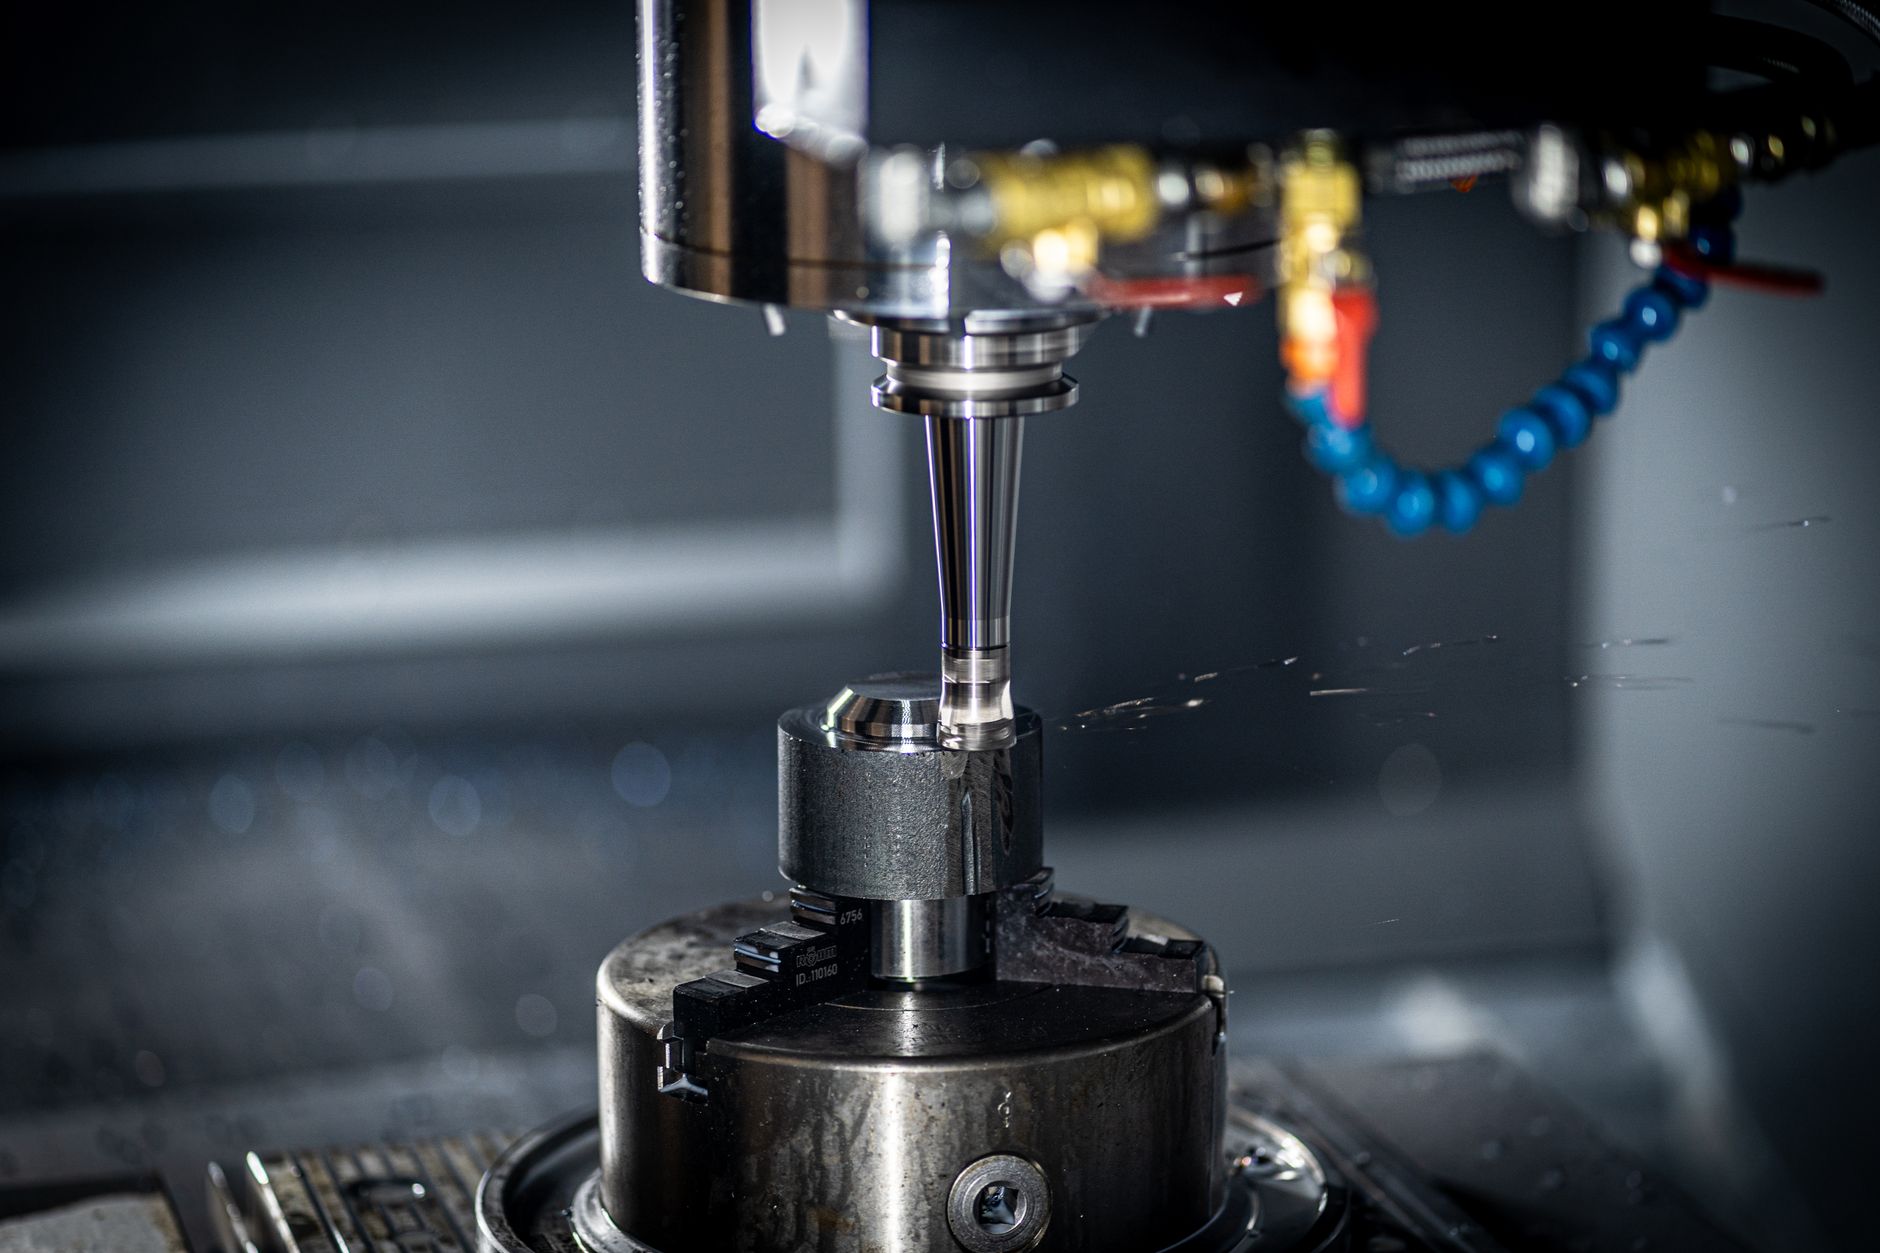
Tapping cuts internal threads in a single pass using a tap tool; thread milling interpolates the same profile with a rotating cutter moving in a helical toolpath, two distinct operations with different trade-offs.
Both processes create threaded holes, but the mechanics are fundamentally different. A tap engages a pre-drilled hole and removes material along a helical path in one continuous motion. A thread mill, by contrast, orbits the hole diameter while advancing axially, tracing the thread profile with a multi-point cutter. Understanding this distinction is the starting point for any tapping threading CNC precision decision. For a detailed comparison of tapped versus threaded holes from a design perspective, see Tapped vs threaded holes in CNC design from Penta Precision.
What Is a Thread Tap and What Are the Core Types Used in CNC Machining?
CNC machining relies on four primary tap types, each matched to specific hole geometry and material conditions.
- Spiral point (gun tap): Pushes chips forward ahead of the tap. Best suited for through holes where chips can exit freely. Common in steel and aluminum production runs.
- Spiral flute tap: Extracts chips upward out of the hole. Designed for blind holes where forward chip ejection is not possible.
- Forming (roll) tap: Displaces material rather than cutting it, producing threads by cold-forming. No chips are generated, making it ideal for ductile metals such as aluminum and copper alloys.
- Straight flute tap: A general-purpose tap used in softer materials and through holes where chip control is less critical.
Selecting the wrong tap type for the hole geometry is one of the most common causes of tool breakage in CNC threading operations. For a comprehensive breakdown of CNC thread tap types and selection guidance, CNC Thread Tap Types Explained from JLCCNC is a useful reference.
What Are the Key Differences Between a Tapped Hole and a Thread-Milled Hole in Terms of Quality and Application?
Tapped holes are produced faster and suit high-volume runs; thread-milled holes deliver tighter pitch accuracy and better surface finish control where tolerance is the priority.
Thread milling also gives the machinist independent control over hole diameter and thread profile, a single tool can cut multiple thread sizes, and climb or conventional milling direction can be adjusted to improve finish. Tapping offers no such flexibility once the tap is selected.
Three part-design factors determine which process is appropriate before any tool is chosen: thread engagement length, hole depth relative to diameter, and material ductility. Deep blind holes in hard alloys, for example, create chip evacuation and torque conditions that often make thread milling the safer choice, while shallow through holes in aluminum favor a forming tap for speed and thread strength.
Main Methods for Creating Internal Threads on a CNC Machine
CNC machines produce internal threads through four primary methods: rigid tapping, tension-compression tapping, thread milling, and thread forming, each suited to different materials and tolerance requirements.
Pros and Cons of Different Internal Threading Methods in CNC Machining
Rigid tapping synchronizes spindle RPM directly with Z-axis feed rate, eliminating the need for a floating holder. The machine controller matches spindle rotation to axial movement at a fixed ratio, which means the thread pitch is governed by the machine itself rather than mechanical compliance. For tapping threading CNC precision applications, this synchronization is critical, any mismatch between spindle speed and feed produces pitch errors that compound across a production run.
Tension-compression tapping uses a floating holder that absorbs small feed discrepancies. It is more forgiving on older CNC equipment where rigid tapping synchronization is less reliable, but it introduces a small amount of mechanical play that limits pitch accuracy in tight-tolerance work.
Thread milling uses a multi-point cutter moving in a helical path to generate the thread profile. It handles blind holes cleanly, allows a single tool to cut multiple thread sizes, and leaves no broken tap risk. The trade-off is longer cycle time and the need for more complex CAM programming.
Thread forming (roll tapping) displaces material rather than cutting it. This cold-working action produces stronger thread walls because the grain structure flows rather than fractures, making it the preferred choice for ductile materials like aluminum and mild steel. Chip-producing cut taps remain the correct choice for brittle materials such as cast iron, where material displacement would cause cracking.
How Material-Specific Tapping Parameters Vary for Exotic Alloys
Titanium and nickel-based alloys like Inconel present specific challenges that standard tapping parameters cannot handle. Both materials work-harden rapidly under cutting pressure, meaning a tool that dwells or slows generates heat that hardens the material ahead of the cutting edge, accelerating tool wear and risking tap breakage.
For these alloys, lower surface speeds reduce heat buildup at the cutting edge. High-pressure coolant directed at the tap flutes clears chips before they re-enter the cut and provides thermal control. Tap geometry also matters: a higher helix angle improves chip evacuation in deep holes, while a spiral point pushes chips forward in through-hole applications. Selecting the wrong geometry in titanium or Inconel typically results in chip packing and tap failure rather than a recoverable surface finish issue.
How to Choose the Right Tap Type and Tapping Method for Your Part
Tap selection depends on four variables: hole type, workpiece material, required thread standard, and whether your CNC machine supports rigid tapping.
How to Select the Right Tap for Blind Holes
Blind holes require spiral flute taps. The helical flutes pull chips upward and out of the hole during cutting, preventing chip packing at the bottom—a condition that causes tap breakage and scrapped parts. Spiral point taps (also called gun taps) push chips forward into the hole, which works in through-hole applications but creates a dead-end chip jam in blind holes.
Thread engagement length also drives tap selection. Engineers typically target an engagement ratio of 1× to 1.5× the thread diameter. Drop below 1× and the joint is prone to pull-out failure under load. Exceed 2× and the cutting torque rises sharply, increasing the risk of tap breakage—especially in harder alloys or small-diameter threads.
Tap coatings extend tool life by addressing the dominant failure mode for each material family. Titanium Nitride (TiN) adds surface hardness and reduces friction in mild steels. Titanium Carbonitride (TiCN) increases hardness further and suits abrasive materials like cast iron. Titanium Aluminum Nitride (TiAlN) excels in high-temperature cutting—its aluminum oxide layer forms at the tool surface during machining, insulating the substrate in stainless steel and hardened alloys.
Engineering Recommendations for Reliable and Repeatable CNC Tapping
For tapping threading CNC precision work, follow this selection sequence before ordering tooling:
- Identify hole type, through or blind. Blind holes require spiral flute taps; through holes accept spiral point taps.
- Determine material class, aluminum, mild steel, stainless, or hardened alloy. Match the tap coating to the dominant failure mode: heat for stainless, abrasion for cast iron.
- Check the required thread standard, metric (M-series), UNC, or UNF. Confirm pitch and tolerance class (6H is the standard metric fit for most fastener applications).
- Select tap geometry, spiral flute for blind, spiral point for through, forming tap where material ductility allows and no chip evacuation is acceptable.
- Confirm CNC machine capability, rigid tapping synchronizes spindle speed and feed rate precisely, eliminating the need for a floating holder. Verify your machine control supports it before specifying tight-tolerance threads.
- Choose holder type, rigid holder for machines with synchronized tapping; tension-compression holder where spindle synchronization is unavailable or marginal.
GC INDUS applies this decision sequence across CNC milling and turning operations, holding thread tolerances to ±0.001mm on production runs for medical device and OEM customers who cannot accept fit variation between batches.
Most Common Tapping Problems in CNC Precision Machining and How to Prevent Them
Tap breakage, poor thread form, and missed inspection steps are the three failure modes that derail tapping threading CNC precision work most often.
What Causes Tap Breakage and How to Prevent It
The pre-drill diameter is the first variable to verify. A hole drilled too small forces the tap to remove excess material, spiking torque beyond the tool’s rated limit. A hole drilled too large reduces thread engagement depth, weakening the joint under load. Most thread standards define the correct tap drill size based on the target thread percentage, typically 75% engagement for steel and aluminum.
Coolant flow is the second critical factor. Without adequate coolant pressure at the cutting zone, heat builds at the tap’s flutes, the workpiece material expands thermally, and the tap seizes mid-cycle. This is especially pronounced in stainless steel and titanium, where work-hardening accelerates as cutting temperature rises.
Blind holes introduce a third failure mode: chip compaction. Chips have nowhere to exit, so they pack at the bottom of the hole. Torque spikes sharply, and the tap snaps. Spiral flute taps direct chips upward and out of the hole rather than downward into the pocket. Pairing spiral flute geometry with peck-tapping cycles, where the tap periodically retracts to clear chips, eliminates most compaction events.
Thread Quality Metrics and Inspection Procedures for CNC-Tapped Holes
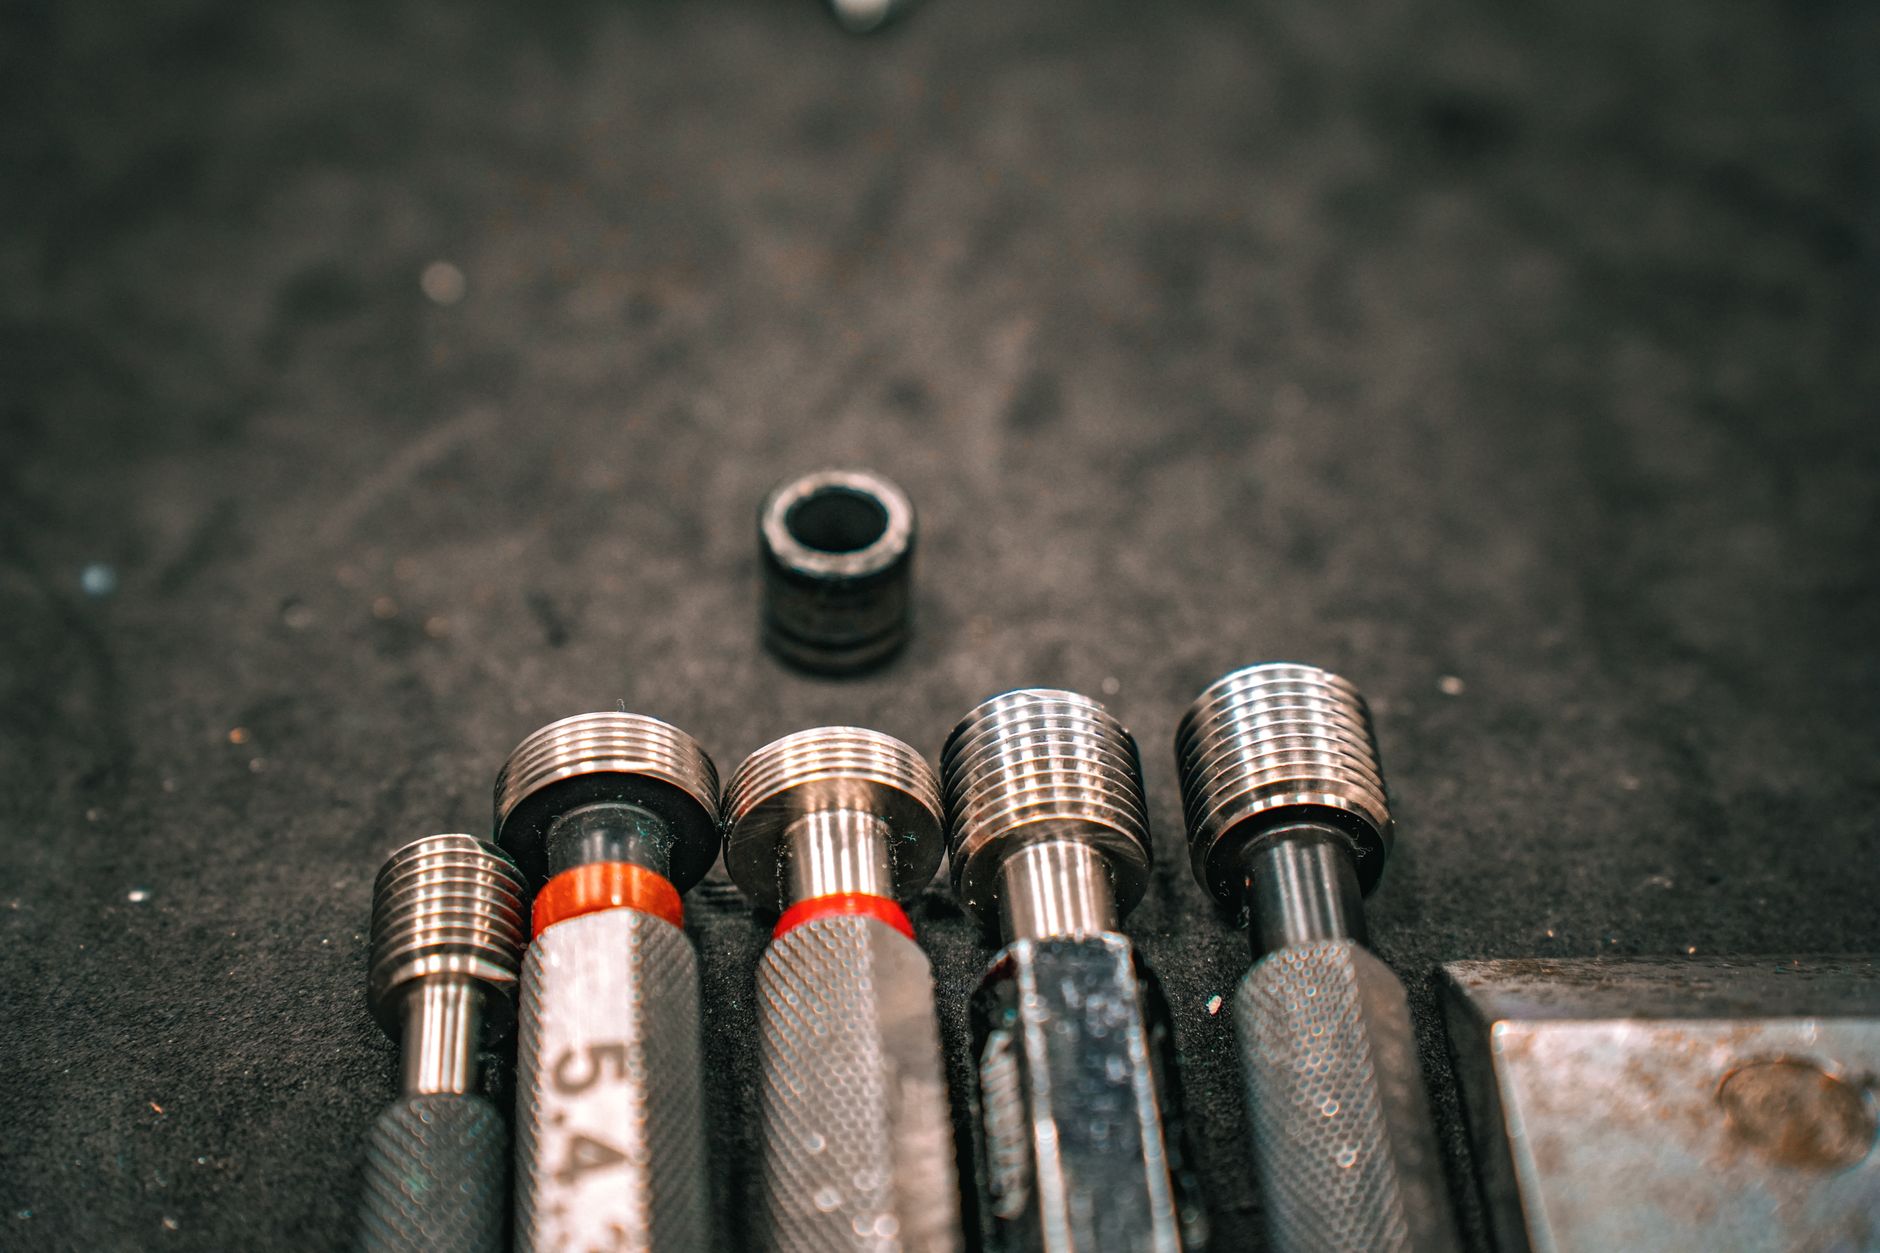
Three metrics define a correctly tapped hole: pitch diameter accuracy, thread form completeness, and surface finish within the thread. Pitch diameter determines whether a fastener will assemble correctly, a go/no-go gauge confirms the diameter sits within tolerance without requiring CMM time on every part. Incomplete thread form, caused by a worn or chipped tap, reduces the load-bearing area of each thread helix. Rough surface finish inside the thread increases friction during fastener installation and reduces fatigue life in cyclic-load applications.
A practical inspection sequence runs in three stages. Before machining, verify the drill diameter against the thread specification, inspect the tap for visible wear or chipping, and confirm coolant pressure at the spindle. During machining, monitor the CNC controller’s torque feedback, a rising torque trend across a batch signals tap wear or chip buildup before breakage occurs. After machining, apply go/no-go gauges to every tapped hole in structural or safety-critical parts. For medical device components, where GC INDUS operates under ISO 13485, optical measurement or CMM thread inspection confirms thread form geometry to the drawing specification.
Tapping Versus Thread Milling: When to Use Each and How Production Volume Affects the Decision
Tapping completes a thread in one tool engagement and is faster per hole; thread milling takes longer per hole but offers geometry flexibility and eliminates catastrophic tool failure risk.
In tapping threading CNC precision work, the speed difference is real and measurable. A tap enters a pre-drilled hole, cuts the full thread profile in a single pass, and retracts, the entire cycle takes a fraction of a second per hole at production feed rates. A thread mill, by contrast, follows a helical interpolation path around the hole diameter, which takes longer per feature. That per-hole time penalty adds up quickly across a high-volume run.
How Production Volume and Part Geometry Affect the Tapping vs. Thread Milling Decision
At high volumes, tapping’s speed advantage compounds, but so does its risk. A single broken tap mid-run can embed in the workpiece, scrap the part, and halt the machine while the tap is extracted. Thread milling avoids that scenario entirely: a worn cutter degrades gradually, producing threads that drift out of tolerance before the tool breaks, giving the operator time to intervene.
Tooling inventory is another factor. One thread mill can produce multiple thread sizes within a compatible diameter range, because the helical path is programmed, not fixed. Tapping requires a dedicated tap for every thread size and pitch combination, a meaningful cost and storage consideration when a part family uses six or eight thread specifications.
Worn taps introduce a specific assembly risk: an undercut thread profile reduces fastener pull-out strength, and a poorly synchronized tapping cycle can produce a mismatched pitch that causes cross-threading during installation. Thread milling, because the cutter path is fully interpolated, does not carry the same synchronization sensitivity.
The decision framework is straightforward. Tapping suits high-volume, single-thread-size runs in standard materials like aluminum or mild steel. Thread milling suits low-to-mid volume production, hard or exotic materials, large-diameter threads, and any part where a broken tool lodged inside the workpiece is an unacceptable outcome, such as a medical implant component or a structural aerospace fitting. GC INDUS applies both processes, selecting based on material, thread specification, and volume to hold tolerances to ±0.001mm across the finished part.
Frequently Asked Questions
What drill size should I use before tapping a hole in CNC machining?
Use a tap drill sized to leave roughly 75% thread engagement, the specific diameter depends on the thread pitch and material. For a standard M6×1.0 thread, that means a 5.0mm drill. Tap drill charts, published by tool manufacturers such as Kennametal and Sandvik, list the correct diameter for every thread size and pitch. Going too small risks tap breakage; too large reduces holding strength.
Can CNC machines tap threads without a floating tap holder?
Yes, rigid tapping, also called synchronous tapping, allows a CNC machine to tap without a floating holder by synchronizing spindle rotation precisely with Z-axis feed rate. Most modern CNC machining centers support rigid tapping as a standard function. It produces more consistent thread depth than floating holders and is the preferred method when cycle time and repeatability matter.
What is the difference between a forming tap and a cutting tap, and when should I use each?
A cutting tap removes material to create thread geometry; a forming tap displaces material by cold-working it, leaving no chips. Forming taps produce stronger threads with better surface finish and are well-suited to ductile metals like aluminum, copper, and mild steel. Cutting taps handle a wider material range, including cast iron and hard steels, where the material is too brittle to form without cracking.
How do I remove a broken tap from a precision CNC part without scrapping it?
EDM (electrical discharge machining) is the most reliable method, it erodes the tap without applying mechanical force to the surrounding material, preserving the hole geometry. Tap extractors work on larger broken taps with exposed flutes, but they risk further damage in tight bores. For high-value precision parts, EDM removal is the standard approach; GC INDUS operates EDM equipment in-house, which means broken-tap recovery can be handled without outsourcing the part to a third party.
How does thread tolerance class affect CNC tapping and part assembly?
Thread tolerance class defines the allowable variation in pitch diameter and controls how loosely or tightly a fastener fits the tapped hole. In metric threading, 6H is the standard tolerance class for most general fastener applications, offering a reliable fit without excessive clearance. Tighter classes such as 5H reduce play but demand more precise tap geometry, better machine synchronization, and closer inspection. Choosing the wrong tolerance class can cause assembly interference or insufficient clamping force in service.
Conclusion
Thread quality in CNC machining comes down to three decisions made before the spindle turns: the right tap type for the material, the correct pre-drill diameter for the thread engagement you need, and a tapping method, rigid or floating, matched to your machine’s capability. Get those three right and thread failures become rare rather than routine.
If your parts require threaded features alongside tight dimensional tolerances, verify that your supplier holds ISO 9001 or ISO 13485 certification and runs in-house inspection on every threaded feature, not just spot checks. A supplier who can also handle EDM, surface treatment, and assembly under one roof eliminates the handoff risk that causes most thread-related quality escapes.
Start by reviewing your current tap drill chart against the actual thread engagement your design requires, that single check catches the most common source of thread failures before a part is ever cut.
Recommended Articles
Explore more from our content library:


